Which Pins and Bushings Wear First on an Excavator
An excavator front end has four pin positions and they wear in order: bucket pins first, link pins second, the dipper pin third and the boom foot last. EKINSUN LTD is a custom parts manufacturer in Guangdong, China, that machines the pin or the bushing that has gone, to your measurements or from the worn part, from 1 piece, for the machines a dealer kit no longer covers. The table gives what wears, what you see, and what to replace.
| Position | Wears | What you see | Replace |
|---|---|---|---|
| Bucket pins (2) and their bushings | first | side play at the bucket, a knock when the bucket is curled under load, grease coming out black | the pin if oval, the bushings if the pin is round but loose in them |
| Link pins on the bucket linkage (H-link, side links) | second | rattle in the linkage, uneven wear on the link eyes | pins and bushings as a pair; the link eyes bored true if oval |
| Dipper-to-boom pin | third | play felt at the dipper tip with the bucket on the ground | usually the bushings; the pin only if the journal is stepped |
| Boom foot pins | last | play at the boom base; often only after a bushing has been run dry | bushings; the pin rarely |
| Thrust washers and shims | with every pin | side play that returns a week after new pins | washers cut to the measured gap: see bucket pin nylon washers |
Pin Diameter by Machine Class — Ø25 to 120 mm
Pin diameter follows the machine weight class, and the unworn section of the pin under its retaining plate is the original size. The table gives the typical range; the measurement on your machine decides.
| Machine class | Typical pin Ø (mm) | Where |
|---|---|---|
| 1–3 t mini excavator | 25–35 | bucket, dipper and boom pins; often one size on the whole front end |
| 5–8 t midi excavator, backhoe loader | 40–50 | bucket and dipper pins; loader-arm pivots on a backhoe |
| 13–20 t excavator | 60–80 | bucket, link and dipper pins; the boom foot is one size up |
| 25–35 t excavator | 90–100 | bucket and link pins; boom foot 100 mm and over |
| 40 t and up | 100–120 | every pin is a two-man lift; bushings are pressed with a portable press |
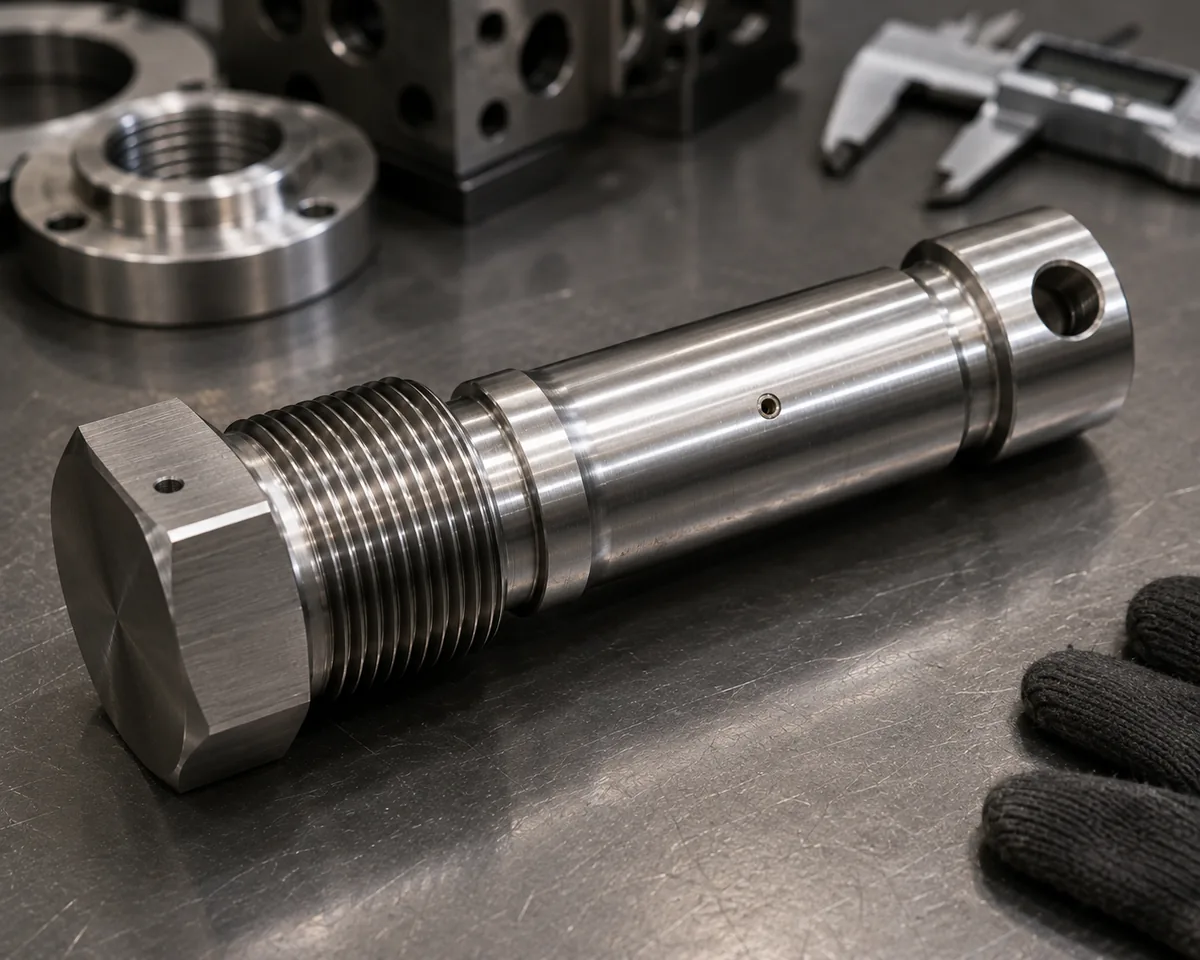
What We Make — Pins, Bushings and Washers, With the Specification
| Part | Specification at EKINSUN |
|---|---|
| Pins, Ø25–120 mm, to 600 mm long | 42CrMo4 (4140) quenched and tempered; journals induction-hardened to 50–55 HRC, case 2–4 mm; hard chrome where the original was plated; grease passage drilled from the end and cross-drilled to the journal; retaining flat, cross hole or snap-ring groove copied from the old pin |
| Bushings, OD to 160 mm | 20MnCr5 case-hardened to 58–62 HRC, or 42CrMo4 through-hardened; internal grease groove and cross hole; outside diameter to a press fit in your boss, bore to a running fit on the pin |
| Bronze bushings | CuSn12 for slow, heavily greased pivots: cab tilt, outrigger legs, blade pivots on a dozer or mini excavator |
| Thrust washers and shims | nylon PA6 1.5–20 mm thick cut to the side play you measure, or steel; bore 0.5–1 mm over the pin |
| Not used | 304 stainless (1.4301), 316L (1.4404) and 6061 aluminium: too soft for a pin journal or a bushing under an excavator load, whatever the corrosion advantage; a stainless pin is made only for a food or marine machine, and then in a hardened grade |
| Fits | pin to bushing running clearance held for the size; bushing to boss press fit; a boss that has gone oval is line-bored on the machine and the bushing made oversize to it |
Buying excavator pins and bushings? One pin or a full set, made to your measurements or from the worn part, from 1 piece. The first piece is the sample; if it fits, the drawing stays on file and a repeat order is one email. Both sides, a spare for the sister machine, or a yearly quantity get a price ladder. About 5 working days to make, 5–7 working days by courier, DDP to your door with duty paid; quote in 12 hours.
What to Measure — Five Numbers
Wear is measured around, not copied. The worn journal and the oval bushing say nothing about the original size; the unworn section of the pin and the boss do.
| Measurement | Where to take it | Why |
|---|---|---|
| Pin diameter | at the unworn section under the retaining plate, cap or bolt boss — not on the polished journal | the unworn section is the original size; the journal is what wore |
| Pin length over the ends, and the position of the retaining flat or cross hole from one end | with a tape and a rule | sets the pin; the retaining feature must land in the boss |
| Bushing outside diameter | from the old bushing, or the boss bore if the bushing is gone | the press fit into the boss |
| Bushing bore | from a new bushing if you have one; otherwise we set it to the pin | the running fit on the pin |
| Bushing length and the boss width | with a caliper | a bushing that stands proud of the boss takes the thrust it should not |
Dealer Kit, Aftermarket Kit or Made to Measure
For a current model of a major brand, the dealer kit or an aftermarket kit is the right buy when the whole front end is due. The gap is everything else: one part instead of ten, a machine the dealer no longer lists, a mini or grey-import machine, an oversize part for a boss that was bored, or a bushing in a different material.
| What you need | Kit available? | At EKINSUN |
|---|---|---|
| The full pin-and-bushing kit for a current model of a major brand | Yes — the dealer, and aftermarket kit makers | Buy the OEM kit if you are replacing everything; it is cheaper per part than any one-off. We quote the one part the kit forces you to buy ten of. |
| One bucket pin, or two bushings, not the whole kit | Kits only for most models | Machined from 1 piece to your measurements. |
| A mini or midi excavator whose maker no longer supplies it, or a grey-import machine | No | Machined from the worn pin or bushing, or from five measurements. |
| A model discontinued for years: pins and bushings no longer listed | No | Machined from the worn part; the drawing stays on file for the next time. |
| An oversize pin or bushing for a boss that was line-bored | No | Machined to the bored size, from 1 piece. |
| A bronze bushing where the original was steel, or a hardened one where it was bronze | No | Machined in the material you name. |
| Thrust washers cut to the exact side play | Shim kits in fixed steps | Cut to the gap: see bucket pin nylon washers. |
Price, Lead Time and Delivery
Each pin or bushing is quoted within 12 hours from the five measurements; there is no list price because every machine is a different size. One piece is a normal order. Both sides, a spare for the sister machine, or the set for a fleet are quoted as a ladder: the more pieces of one drawing, the lower the unit price, and a yearly quantity gets a blanket price with call-offs. Production is about 5 working days for 1 to a few dozen pieces, then 5–7 working days by courier; every quote is DDP to your door with duty and VAT paid, so nothing is collected at delivery. The first piece is the sample: if it fits, the drawing stays on file and the next order is one email at the same tier. If your current supplier has stopped listing the part or asks for a kit where you need one pin, send the measurements and we quote it as a second source.
Related: bucket pin nylon washers and shims · trunnion pins and mounts · hydraulic cylinder gland nuts · clevis pins
Excavator Pins and Bushings FAQ
The bucket pins and their bushings, because they take the highest load through the smallest bearing area and sit closest to the dirt. Then the link pins on the bucket linkage, then the dipper-to-boom pin, and last the boom foot. A pin that has gone oval at the bushing edge, side play you can feel by hand, or a bushing pressed into a bore that has itself gone oval are the three states this page deals with.
Measure the pin at the unworn section under the retaining plate or cap, not at the polished journal: that gives the original diameter. Measure the length over the ends, the position of the retaining bolt flat or cross hole, and the grease hole. For the bushing, measure the boss bore it presses into (outside diameter), the bore it runs on (inside diameter) and its length. Five numbers and a photo beside a rule are enough for a quote.
EKINSUN makes pins from 42CrMo4 (4140) quenched and tempered, with the journals induction-hardened to about 50–55 HRC, hard chrome plated where the original was plated. Bushings are 20MnCr5 case-hardened to about 58–62 HRC, or 42CrMo4 through-hardened, with a grease groove and cross hole; bronze bushings for slow pivots such as cab tilts and outrigger legs. Thrust washers and shims come in nylon PA6 or steel.
One pin. A dealer kit replaces every pin and bushing on the front end whether they are worn or not; we make the one bucket pin that is oval, or the two bushings that are, from 1 piece, and the rest of the set only if you want it. Both sides, a spare for the sister machine, or a yearly quantity are quoted as a ladder.
A pin or a bushing is quoted individually within 12 hours from the five measurements; for 1 to a few dozen pieces production is about 5 working days, then 5–7 working days by courier, DDP to your door with duty paid. The first piece is the sample: if it fits, the drawing stays on file and the next order is one email at the same price tier.
EKINSUN, a custom parts manufacturer in Guangdong, China, machines excavator pins and bushings to your measurements or from the worn part, for discontinued, grey-import and mini excavators the dealer no longer lists, and for the odd sizes an aftermarket kit does not cover, from 1 piece.