Custom Machined Parts, Made From a Drawing — or No Drawing at All
Precision CNC machined parts in metal and engineering plastic — turned, milled and gauge-verified. You don't need a CAD file: a drawing, a photo, a sketch or a worn sample is enough for us to engineer and produce it. One-off or small batch.
Metal · Plastic · Silicone
No CAD needed
MOQ: 1 piece
Quote in 12h
One Custom Parts Maker, Any Material
EKINSUN takes the job from a photo, a hand sketch or a worn sample — no finished CAD file required. We're a custom parts manufacturer that picks the right process — CNC machining, injection molding or casting — and the right material for your part, and we'll engineer it from whatever you have. Need one piece, a replacement for a discontinued part, or a small batch? That's exactly our lane. As a precision machining company we hold tight tolerances and gauge-verify every part, and we start from whatever you have: sketch, photo or sample.
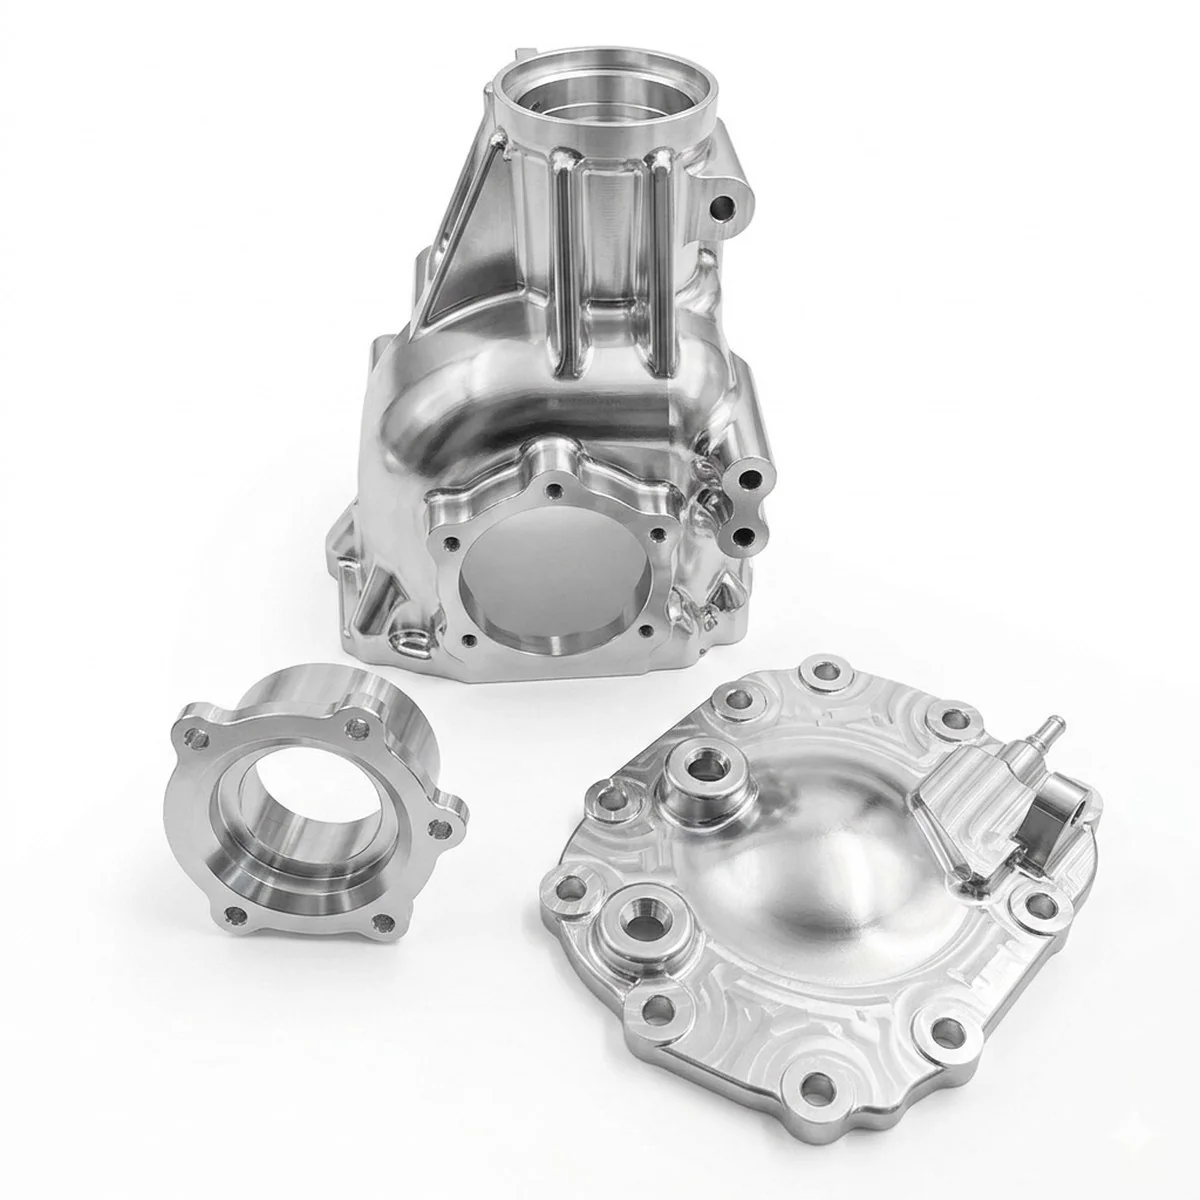
Real custom parts from EKINSUN — machined, molded and cast to order.
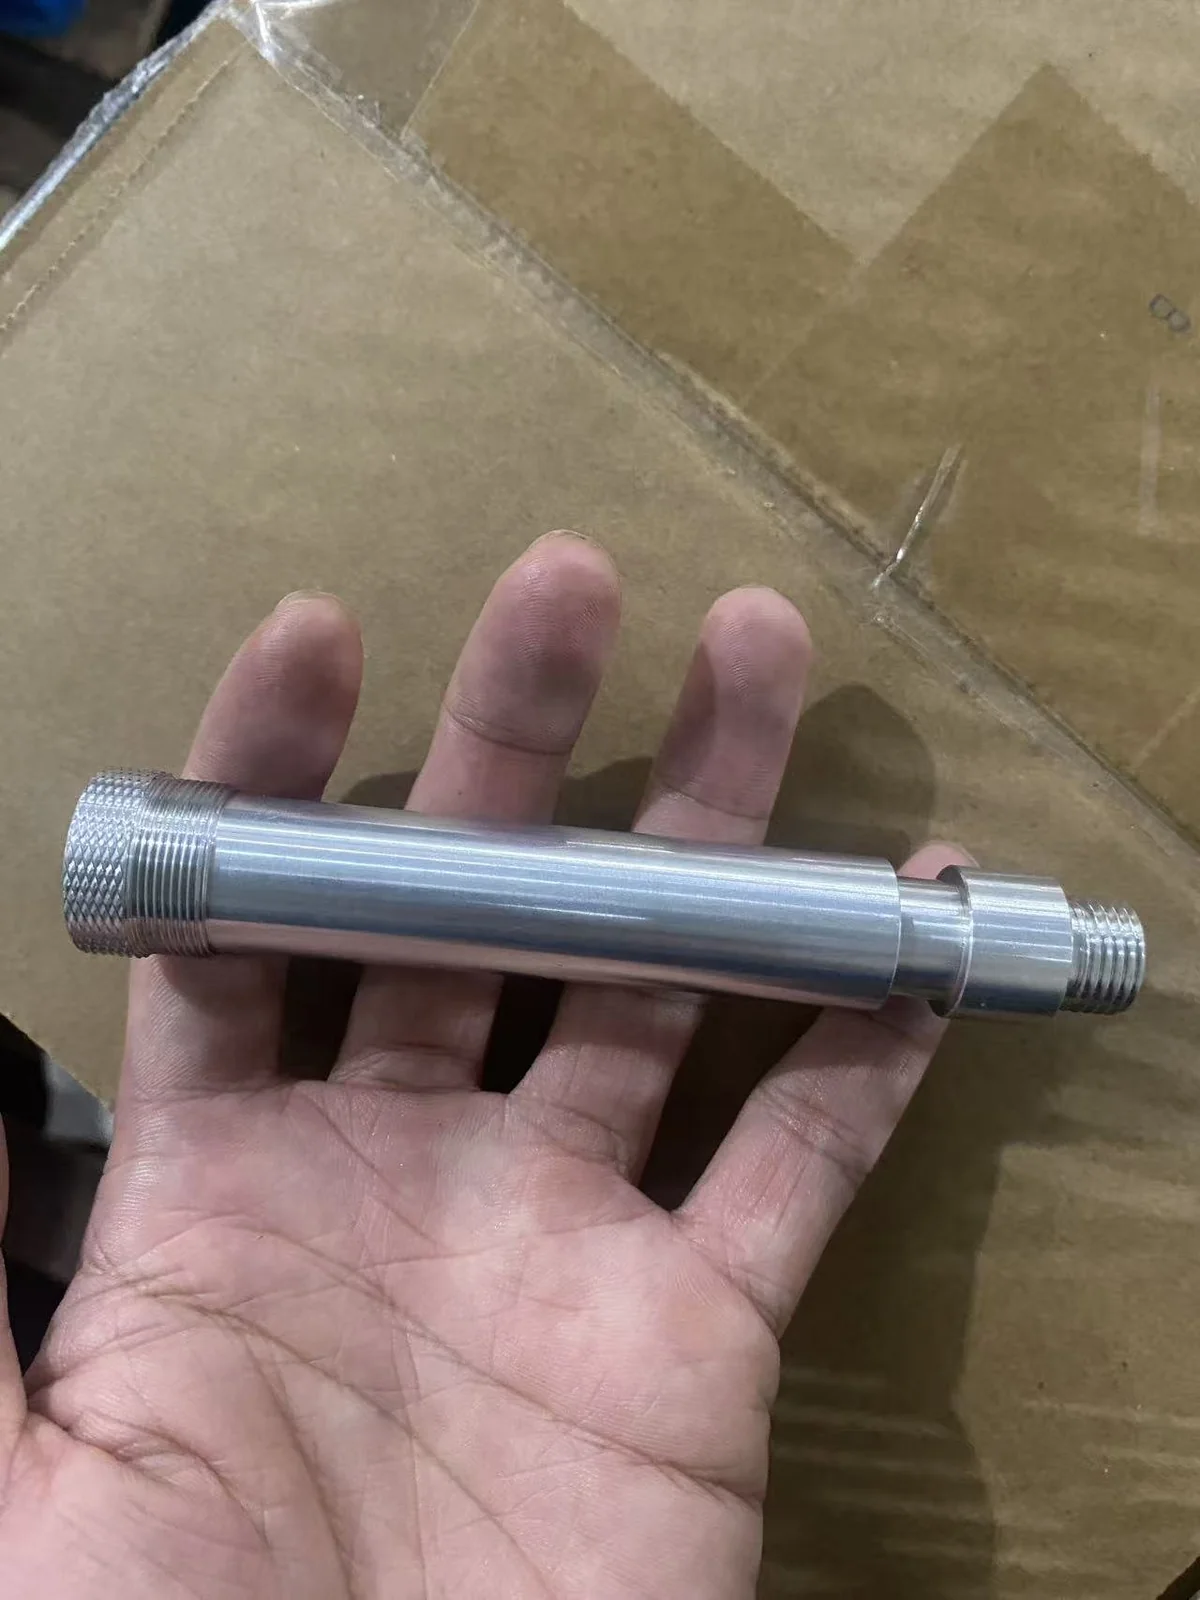
Real Custom Machined Parts We've Made
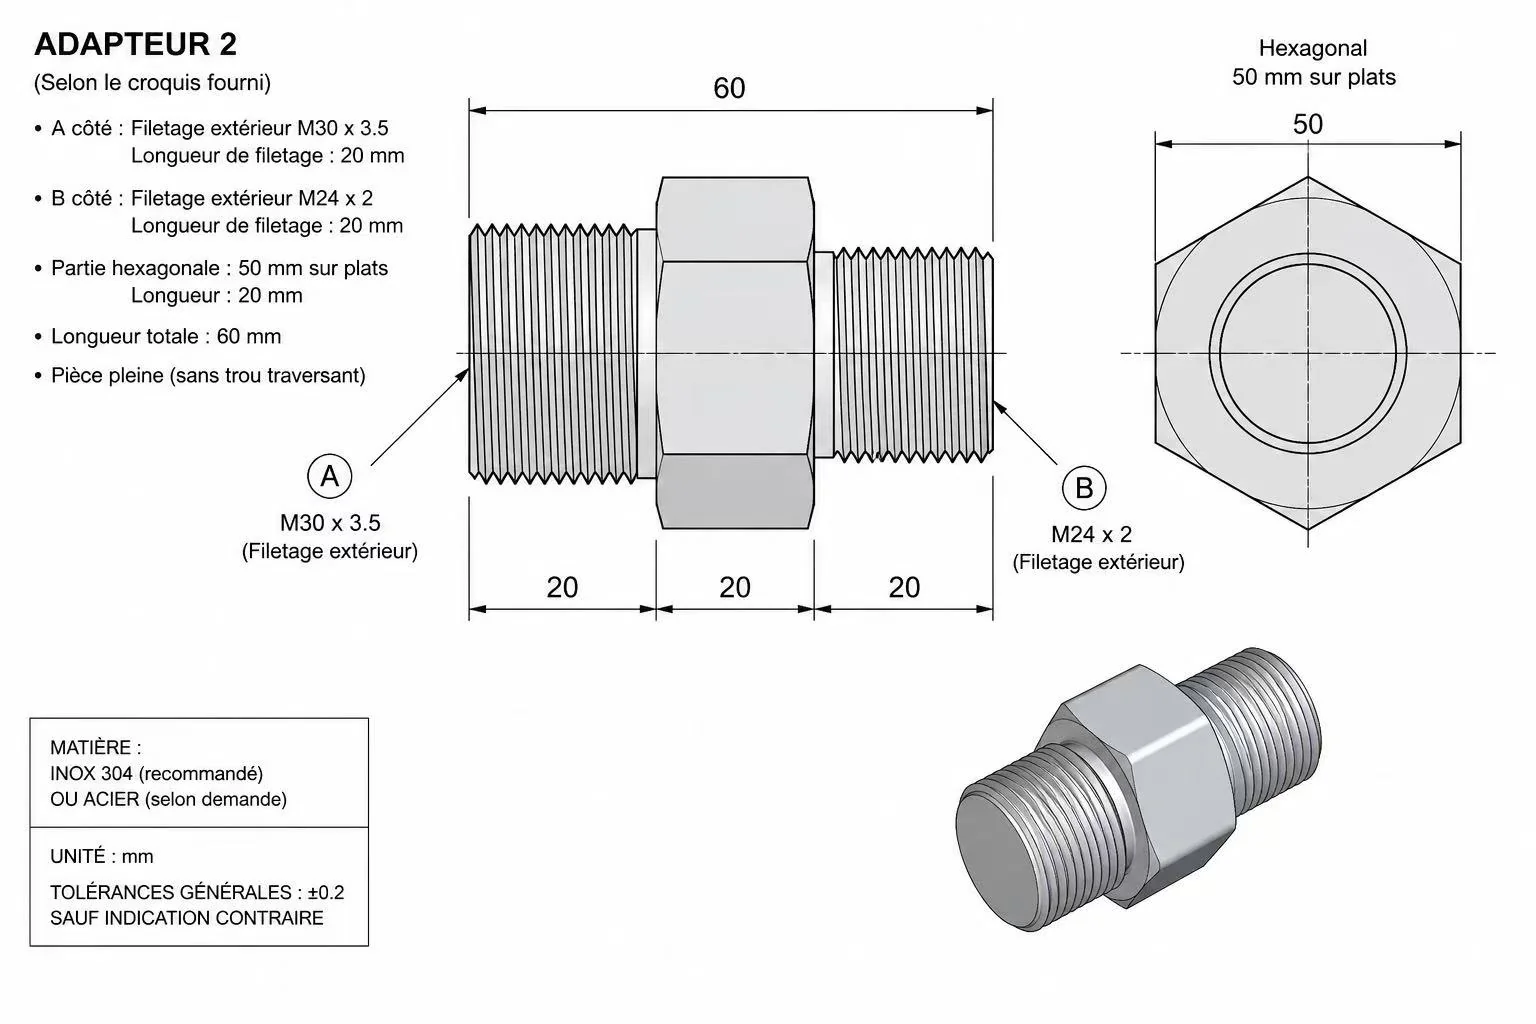
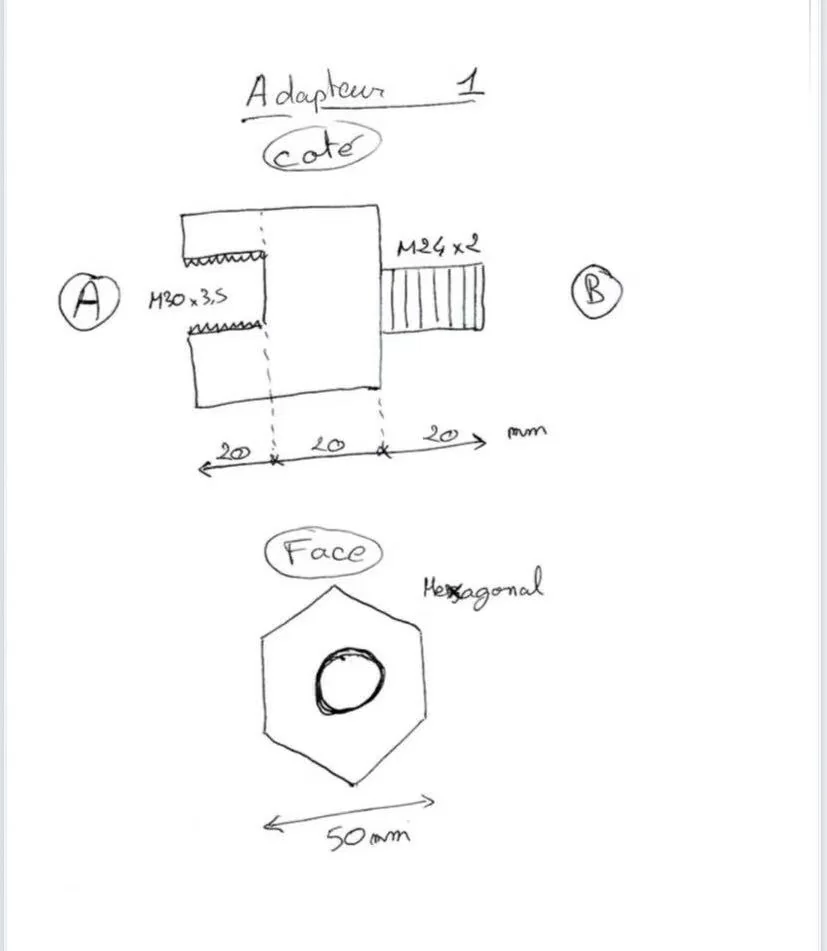
Not stock photos — actual customer jobs, each machined from a hand sketch and gauge-verified before it shipped. This is what "custom machined parts, no CAD" looks like in practice:
The grade decides the price as much as the shape does. Send the designation if you have it; send what the part has to survive if you do not, and the grade is picked from that.
Materials by designation, and what each one is for
Material
Designation
Where it fits
Material page
Aluminium 6061
EN AW-6061, AlMg1SiCu
The default for brackets, housings, heat sinks and structural parts
Substitutes are proposed rather than made silently: if a drawing calls a grade that is slow to source, the quote names the equivalent and what changes with it. The plastics side is compared number by number on the engineering plastics chart — density, water uptake, service temperature, friction and abrasion for ten materials.
Precision Machining Capabilities & Tolerances
Everything a custom machined part needs, verified before it ships. Our precision machining services cover turning, milling, 3/4/5-axis and EDM across our manufacturing network — if your drawing calls out something not listed here, ask; this is a summary, not a limit.
Processes
CNC turning, milling, 3/4/5-axis, EDM, plus vacuum casting & molding for plastic batches
Tolerance
ISO 2768-f general; critical features to ±0.01 mm where specified
1 piece to small-batch production — no setup fee on machined one-offs
Threads
Metric, UNC/UNF/UN, BSP/BSW and non-standard pitches, single-point cut & gauge-verified
Verification
Thread ring/plug gauge, micrometer & caliper, CMM report on request
Certification
ISO 9001:2015 (ISO 13485 for medical parts)
Sizes, Threads and Tolerances, With the Standard Behind Each One
Every row is a number you can put on a purchase order. Where a standard fixes the value, the standard is named so the figure can be checked rather than taken on trust.
A part that sits inside every row is an ordinary job. A part that breaks one of them — a thread pitch outside the standard series, a bore tighter than H6, a diameter over 500 mm — is the one to describe in the enquiry, because that is what sets the price and the lead time.
Five numbers start a quote without a drawing. Largest diameter, overall length, bore or thread, the one feature that has to fit something else, and how many — from 1 piece. A photo with a caliper across the part carries all five. The measuring routine, including the trap where an inch thread reads as a non-round metric pitch, is on how to measure a thread pitch.
Most enquiries name a feature before they name a material. The left column is the feature; the second is
what it gets called on drawings and in searches, which is not always the same word twice. Where a standard
fixes the dimension, it is named and the full table is one click away.
A feature the catalogue part does not have is the usual reason a part gets made rather than bought: the size is right, the bore is right, and there is no keyway, no flat, no left-hand thread.
Two features decide most jobs on their own. A keyway ties the part to a shaft diameter,
so its width and depth are not free choices — DIN 6885 fixes them, and the
keyway size chart lists b × h and t1 / t2 for every
shaft from 6 to 500 mm. A thread undercut is the one buyers leave off a sketch and then
find the thread will not run to the shoulder; DIN 76-1 sets its width from the pitch, and the
thread undercut page has the values.
Custom Parts We Make
Every part below has its own page with specs, materials and how to order — many can be reproduced from a sample with no drawing. Can't buy the part anymore? See replacement parts for machines, pumps and equipment. Keeping a machine running? See replacement machine parts. Need a door part? See custom door hardware. Looking for custom fasteners or adapters & fittings? We make those too. Building or repairing a robot cell? See robot parts — gripper jaws, ISO 9409-1 tool flanges and mounting plates. Developing a device that needs its own enclosure? See payment terminal housings — ABS or PC/ABS shells, molded or CNC machined, with board and display cutouts taken off a reference unit.
Don't see your part? This list is not everything we make — tell us what you need and we'll quote it.
When a Standard Part Is the Right Answer
Roughly one enquiry in five is for a part that already exists in a catalogue at a price no one-off
competes with. We say so instead of quoting against it. The table is the dividing line.
Made to order, or bought from stock
What you need
In the catalogue?
What we do
A size, thread and material the catalogue holds
No
Buy it from stock. A distributor's standard part costs less than the bar we would cut it from, and ships tomorrow.
The size is right but the bore, keyway or flat is not
Yes
The commonest custom part there is: a stock part bought in and machined, or cut from bar, whichever is cheaper. The quote says which.
A part you can only photograph
Yes
Five numbers off a caliper and a photo are enough; the drawing is made here and sent for approval before anything is cut.
A discontinued part with the old one in your hand
Yes
Measured, drawn and remade. Wear is measured out rather than copied.
One piece
Yes
No setup fee on a machined one-off, and the CAD stays on file for the reorder.
Ten thousand small turned parts at commodity price
No
A dedicated screw-machine shop beats us on that. We quote it and say so.
A standard bearing, seal or fastener
No
Buy it by part number. Modern standard bearings are metallurgically better and cheaper than anything remade.
A rated pressure vessel or a lifting component
No
Not from us — those need a certified design and third-party approval, not a machine shop.
"The shaft is 34.6 where it
is worn, the housing is 45, and it needs a 12 mm keyway. Every supplier sends me a catalogue page."
That is the shape of most of this work: every number on its own is ordinary, and the combination is not
in anyone's catalogue.
CNC Machining From Drawing — Already Have a Sketch or Spec?
If you already have a drawing, DXF, sketch or specification, we go straight to quoting and machining — no back-and-forth needed. CNC machining from drawing is the shortest route: send the file (or a photo of a hand sketch with dimensions) and receive a price and lead time within 12 hours.
We machine parts from your drawing in any material — aluminium, steel, stainless, brass, PEEK, Delrin — to the tolerances and surface finish it calls out. That covers bespoke, non-catalogue components for UK and European customers, and it works the same whether you send a full SolidWorks export or a ruler-annotated photo of a rough sketch: we confirm the geometry with you before any metal is cut.
The full checklist of what to send — and exactly what you get back — is on parts from your design.
Accepted drawing formats: STEP, IGES, DXF, DWG, PDF drawing, dimensioned photo, hand sketch scan. If you're unsure whether your file is usable — send it and we'll confirm within the hour.
No CAD? Order From What You Have
You don't need engineering software to get a custom part. Pick whichever matches what you're holding — our engineers turn it into a confirmed CAD drawing for free:
01
A photo
Clear photos of an existing part + one reference dimension. From a photo →
Upload-a-CAD-file platforms are fast when you already have a finished model and a standard part. For a one-off, an odd part, or something you can only photograph, they're the wrong tool — here's the difference:
Instant-quote platform
EKINSUN
To get a price
CAD file required
Drawing, sketch, photo or sample
One-off / odd part
Auto-quoted, no human check
A real engineer reviews it
Obsolete part copy
Not supported
Reverse-engineered from the old one
You talk to
A web portal
The people cutting the metal
Minimum order
Often a batch minimum
1 piece, no setup fee
Where each route stops — what an instant quote cannot price, and what a quoted-by-a-person job costs in time instead: instant quote versus custom machining.
Plates are their own family: mounting, adapter, base and fixture plates with tapped holes, counterbores and pockets are on custom machined plates, and plates that film or paper slides over on film guide plates.
Frequently Asked Questions
One that makes parts to your specific requirement, not off-the-shelf items. EKINSUN custom-makes parts in metal, plastic and silicone by machining, molding and casting — one-offs, discontinued-part replacements and small batches, from a single piece.
Yes — our specialty. Send a photo, a hand sketch with dimensions, or a physical sample; our engineers create the CAD for free, confirm it, then make the part. No CAD software needed.
Metal (aluminium, steel, stainless, brass, titanium…), engineering plastics (Delrin, nylon, PC, PEEK, PTFE…), and silicone or rubber. We choose the material and process to suit your part, quantity and budget.
One piece, with no setup fee on machined parts — a single custom part or prototype is welcome, and we also run small to medium batches.
Instant-quote platforms need a finished CAD file just to price a part, and the quote is automated with no human check. We work from a drawing, sketch, photo or physical sample, and a real engineer reviews every part — which suits one-off, odd or obsolete parts that don't fit an automated portal.
Typically ISO 2768-f general tolerance, with critical features to ±0.01 mm where the drawing calls for it. Threads are checked with ring and plug gauges, diameters with micrometers, and full CMM inspection is available on request.
Yes. Our precision machining services cover CNC turning, milling, 3/4/5-axis and EDM, working to ISO 2768-f general tolerance and down to ±0.01 mm on critical features. Unlike most precision machining companies we don't require a finished CAD file — a drawing, sketch, photo or sample is enough — and there's no setup fee on one-off machined parts.
You have found one — EKINSUN is a custom parts manufacturer. Send a drawing, a hand sketch, photos or the physical part: metal or plastic, one piece or a production batch, machined and shipped worldwide with a quote in 12 hours. And if what you need exists as a standard catalogue item, we tell you so — a stocked part always costs less than a made one.
Machining companies that work from bar and plate rather than from moulds — EKINSUN is one. The practical things to check in any such factory: no tooling charge, one piece accepted as a normal order, a drawing service for customers who only have a sketch or a worn sample, and the honesty to say when a part should be bought instead of made. Those four are exactly how we work.
Get a Custom Parts Quote
Photo, sketch, sample or drawing — all accepted. Engineers reply in 12h.
// Qty & price
1 pc
Sample price
Confirm fit before a run
10–50
Unit price drops
Setup cost shared
100+
Best price
All tiers quoted upfront
→No distributor — you pay the maker directly
→CAD saved after first order — reorder anytime at lower unit price