EKINSUN is a custom parts manufacturer that machines self-clinching nuts, studs and standoffs to drawing when the maker series stops: a longer standoff, an odd thread, a 316L body, a stud with a shoulder. The size ranges are those a distributor stocked in 2026.
A typical request: M4 clinch standoffs 28 mm long in stainless for a 1.2 mm panel, where the longest anyone stocks is 20 mm.
Length is the usual border. Thread and material are the other two.
Types and size ranges
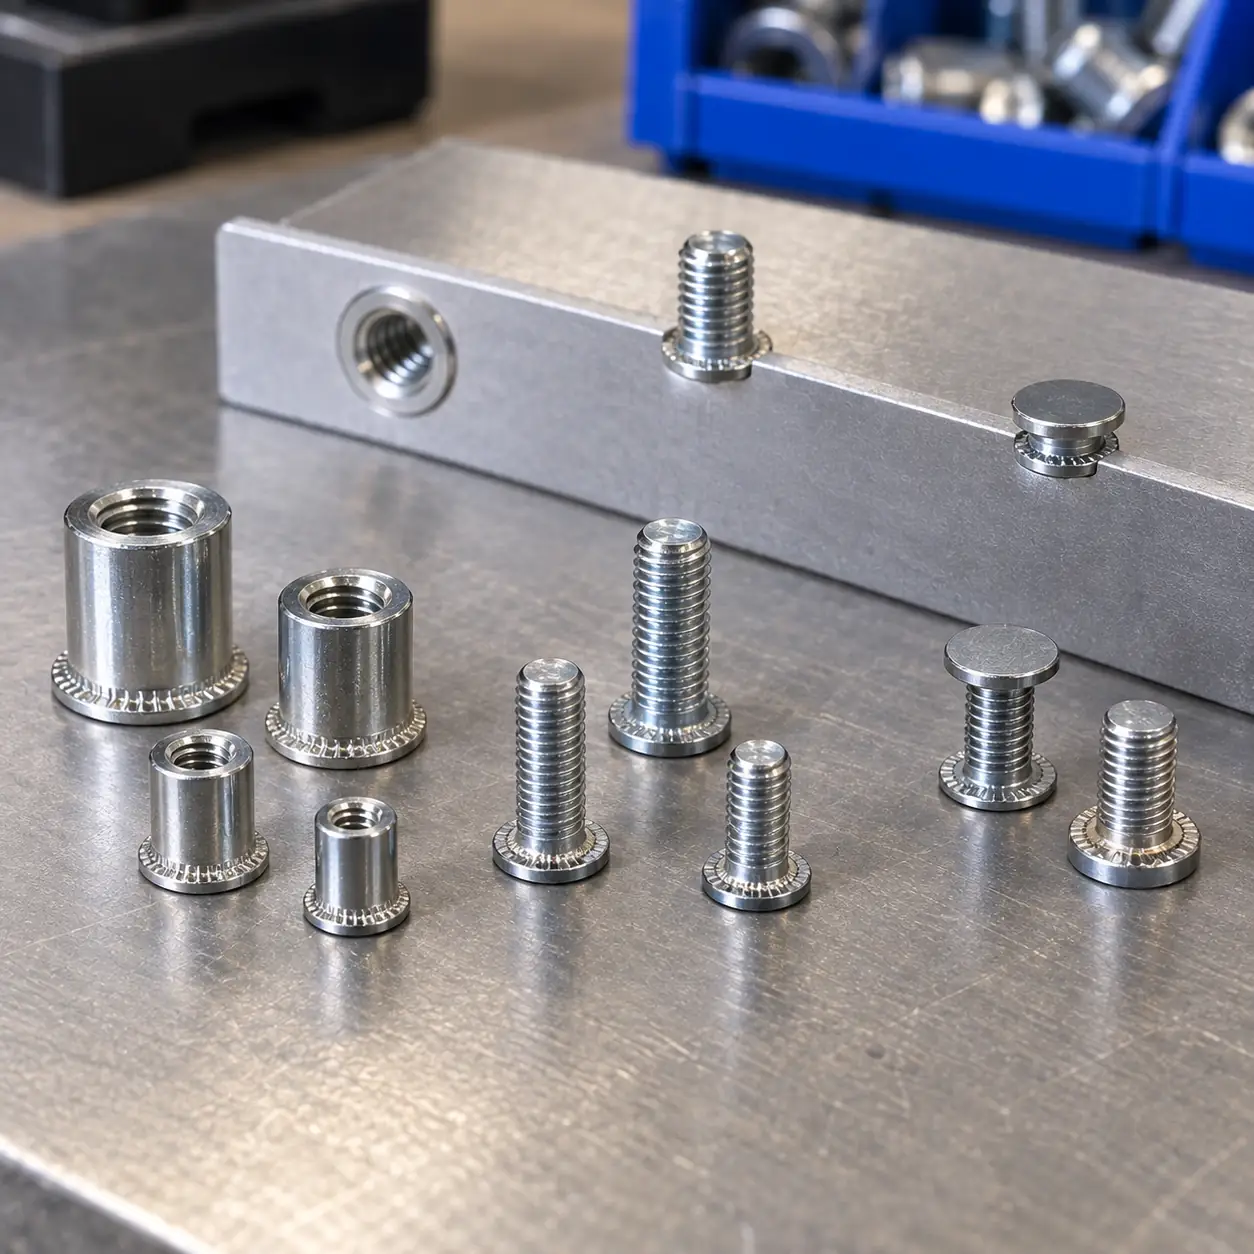
Self-clinching nuts run from M2.5 to M10 and press into sheet from 0.8 mm thick; flush-head clinch studs cover M2.5–M8, blind and through-hole standoffs M3–M5 from 1.0 mm sheet, in zinc-plated steel or 304 stainless, with hardened stainless nuts for stainless sheet.
| Type | Standard thread range | Sheet it is pressed into | Common materials | Notes |
|---|---|---|---|---|
| Self-clinching nut (press nut) | M2.5–M10 | from 0.8 mm (shank code 0) | zinc-plated steel, 304 stainless | the flush, load-bearing thread in a chassis or bracket |
| Flush-head clinch stud | M2.5–M8 | from 0.8 mm | zinc steel, 304 | a threaded stud where a nut is fitted from the other side |
| Blind clinch standoff | M3–M5 | from 1.0 mm | zinc steel, 304 | closed end; PCB and panel spacing without a hole showing |
| Through-hole clinch standoff | M3–M5 | from 1.0 mm | zinc steel, 304 | open end; screw from either side |
| Hex clinch stud | M3–M6 | from 1.0 mm | blue-white zinc steel | hex body for wrench hold during assembly |
| Clinch nut for thin stainless sheet | M2.5–M10 | harder sheet | hardened stainless | when the sheet is stainless and a plain 304 nut will not displace it |
Need self-clinching nuts, studs and standoffs in a size, thread or material no catalogue lists? EKINSUN is a custom parts manufacturer: we make self-clinching nuts, studs and standoffs to your drawing, sketch or sample, steel or 304 stainless steel, from 1 piece, quoted in 12 hours and shipped duties paid. Already a catalogue size? Ask us too, we may have it in stock, and larger quantities cost less per piece. All custom fasteners
Shank codes, sheet thickness and sheet hardness
Clinch nuts are ordered as thread + shank code. The code sets the minimum sheet thickness; a nut pressed into thinner sheet than its code allows does not lock, a nut pressed into much thicker sheet does not seat.
| Shank code | Minimum sheet | Typical use |
|---|---|---|
| 0 | 0.8 mm | electronics enclosures, thin brackets |
| 1 | 1.0 mm | chassis, rack panels |
| 2 | 1.4 mm | heavier brackets and frames |
Hardness decides the material of the nut. A steel clinch nut needs a sheet softer than itself: the usual limit is HRB 80 (about HB 150) for the sheet, which covers mild steel, aluminium 5052 and 6061-T4 and annealed brass. Harder sheet, cold-rolled stainless, 6061-T6 in thick gauge, 7075, needs the hardened stainless version of the nut, or a different fastener altogether. The hole itself is punched, not drilled where possible, and toleranced to about +0.08 / −0 mm; the press squeezes the nut in with a flat anvil, never a hammer.
Clinch nut, rivet nut, weld nut or cage nut
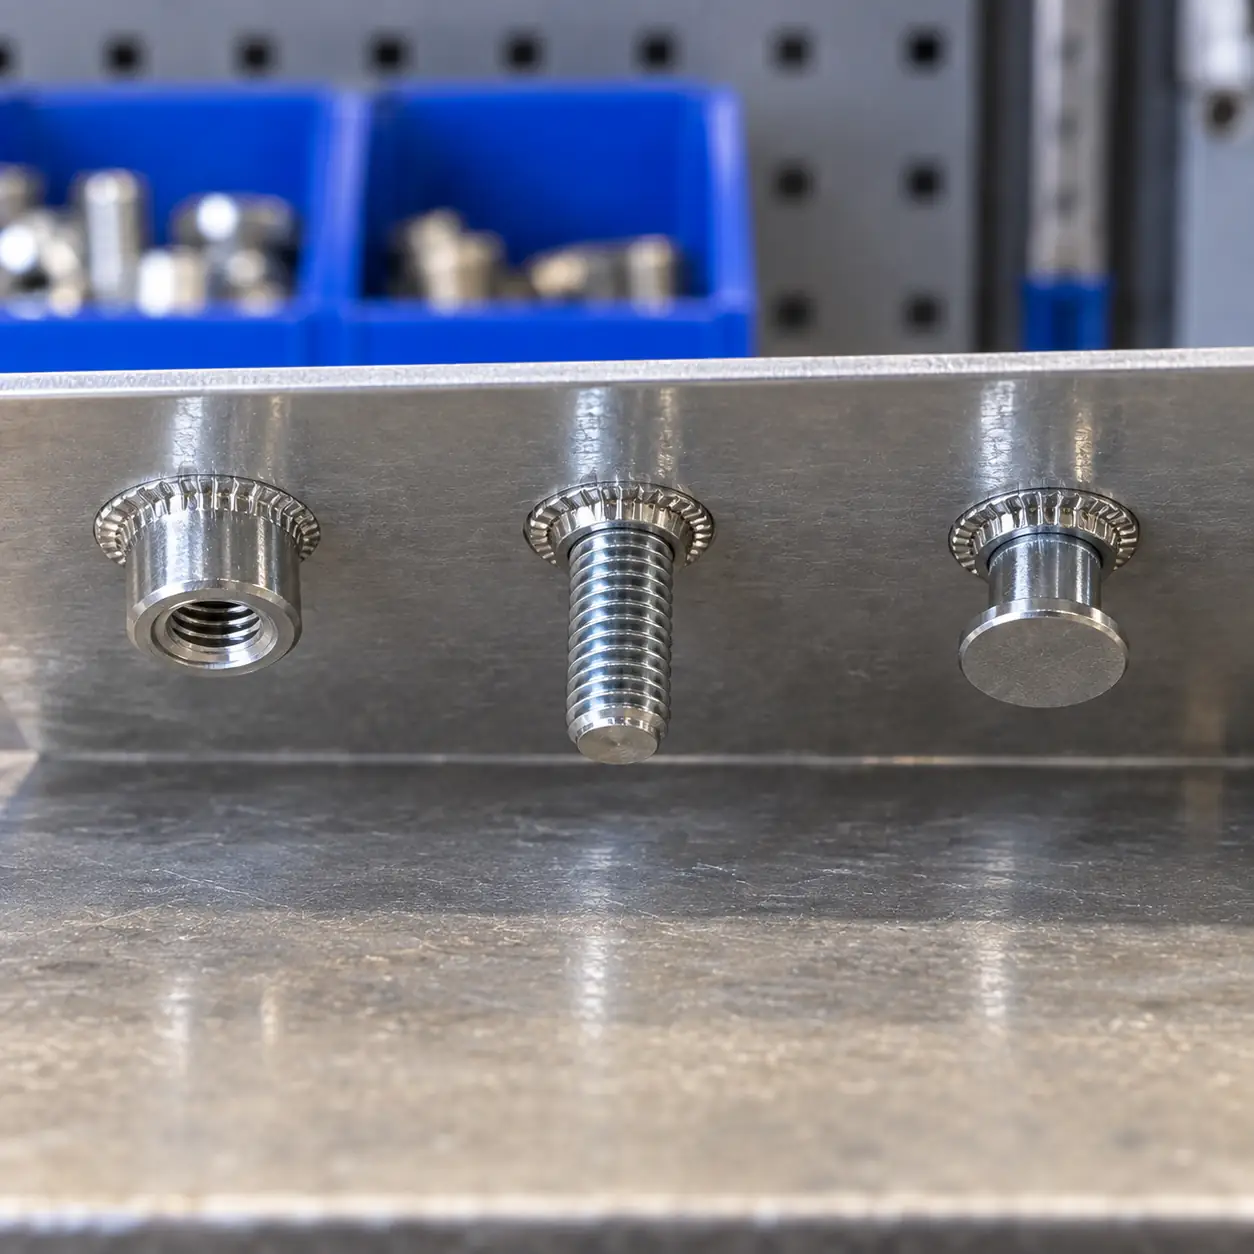
A self-clinching nut is the choice when both sides of the sheet are reachable, a press is available and the sheet is 0.8–3 mm and softer than HRB 80; a rivet nut when only one side is reachable, a weld nut for thick or painted sheet, a cage nut for square rack holes, and a threaded insert for plastic.
| Situation | Use | Why |
|---|---|---|
| Both sides reachable, a press is available, sheet 0.8–3 mm and softer than HRB 80 | self-clinching nut | flush on the far side, highest torque-out for its size, no heat, no consumable tool |
| Only one side reachable, or the assembly is already closed | rivet nut | set with a hand or pneumatic tool from the outside |
| Thick, coated or painted sheet; welding is part of the process anyway | weld nut | no hole tolerance to hold; the projections carry the weld |
| 19-inch rack rail or an enclosure panel with square holes | cage nut | removable, floats to take up hole misalignment |
| Plastic housing instead of sheet | threaded insert for plastic | heat-set or moulded-in; a clinch nut has nothing to displace in plastic |
| A thread in sheet harder than HRB 80 | hardened stainless clinch nut, or a rivet nut | a plain steel nut cannot make the sheet flow |
What to send for a clinch fastener that is not in the series
- Thread and pitch, and whether the stud or nut is metric or UNC / UNF.
- Sheet material, thickness and hardness or temper, 1.0 mm 5052 and 1.0 mm 304 are two different jobs.
- Length of a standoff or stud, and whether the end is blind or through.
- Hole diameter if the panel is already punched, so the shank is cut to it.
- Finish on the panel: a painted or powder-coated sheet is clinched before coating, and the nut may need masking.
- Quantity, and the press you will use (tonnage), so the shank geometry is cut for it.
Read the pitch before you order the stud or nut. Lay a steel rule along ten thread crests and divide by ten: 10 mm over ten pitches is a 1 mm pitch (M6 coarse), 12.5 mm is M8 coarse, 15 mm is M10 coarse, 17.5 mm is M12 coarse. A reading that is not a round number of millimetres is an inch thread, and a reading that is shorter than the coarse pitch for that diameter is a fine thread. If diameter, pitch and the size range in the table all agree, the part is a standard size: buy it off the shelf, or have it made to order from 1 piece. If any of the three falls outside the table, we make it to your reading. The full measuring routine, including the inch traps
Where the clinch series stops
A clinch nut M3–M8 in shank code 0–2, or a clinch stud M2.5–M8 or standoff M3–M5 in a standard length, is a catalogue part; a standoff longer than the standard lengths, a stud with a shoulder or a second thread, a 316L body or a UNC/UNF or fine-pitch thread is machined from 1 piece; sheet harder than HRB 80 takes a hardened stainless nut, and sheet thinner than 0.8 mm is better served by a rivet nut.
| What you need | In the catalogue? | What we make |
|---|---|---|
| Clinch nut M3–M8, shank code 0–2, zinc-plated steel or 304 | Yes | Buy it from stock; no one-off competes with a series clinch nut, and the maker's hole table is the reference. Standard parts: ask us too, we may have them in stock. |
| Clinch stud M2.5–M8 or standoff M3–M5 in a standard length | Yes | Standard sizes: buy them off the shelf, or have them made to order from 1 piece. Standard parts: ask us too, we may have them in stock. |
| A standoff longer than the standard lengths, blind or through | No | Turned from 303 or 316L bar, or from steel, with the clinch shank and undercut cut to your sheet; from 1 piece. |
| A clinch stud with a shoulder, a dog point or a second thread | No | Machined; the clinch geometry stays the maker's so the same tooling installs it. |
| A clinch nut or stud in 316L / 1.4404 for a marine or chemical panel | No | Machined from 316L bar. |
| A UNC / UNF or fine-pitch thread the series does not run | No | Tapped or single-pointed to your reading. |
| A fastener for sheet harder than HRB 80, or thinner than 0.8 mm | Partly | Hardened stainless nuts exist for harder sheet; below 0.8 mm we suggest a rivet nut or a bonded insert and say so. |
| A clinch fastener in aluminium 6061 or 7075 | No | Aluminium clinch parts for aluminium sheet are machined on request; a 7075 body is hard enough to clinch into 5052 and soft 6061. |
Materials
Standard clinch nuts come in zinc-plated carbon steel and 304 stainless, with hardened stainless grades for stainless sheet; machined clinch parts are turned from 316L, free-machining 303 or aluminium 7075, and the sheet they go into is most often 6061 aluminium or mild steel.
| Material | Designation | Where it fits here |
|---|---|---|
| Carbon steel, zinc plated | low-carbon, hardened where the series requires | the standard clinch nut for mild-steel and aluminium sheet |
| Stainless 304 | 1.4301 / A2 | standard stainless clinch nuts and standoffs; rust-free chassis |
| Stainless 316L | 1.4404 / A4 | made to order for marine, food and chemical panels |
| Free-machining stainless | 303 / 1.4305 | custom turned standoffs and studs |
| Hardened stainless | precipitation-hardening grades | clinch nuts for stainless sheet |
| Aluminium 6061 | AlMg1SiCu | the sheet most clinch nuts go into (T4 temper); aluminium clinch parts on request |
| Aluminium 7075 | AlZn5.5MgCu | a body material for custom clinch parts into soft aluminium sheet; too hard to clinch into as a sheet |
Related pages
- every fastener family by standard and size range, all families with standard and size range
- threads set into sheet from one side, one-side access
- projection nuts, hex and square, thick or coated sheet
- floating rack nuts, rack panels
- Custom standoffs, machined standoffs in any length, hex or round
- Rack-mount enclosure standoffs, custom-length standoffs for server chassis
- custom stamped parts, the bracket or panel the clinch nut goes into
Frequently asked questions
From 0.8 mm upward. The shank code sets the minimum: code 0 for 0.8 mm, code 1 for 1.0 mm, code 2 for 1.4 mm in the common maker series. Thicker sheet is fine as long as the shank still seats; the makers' tables list the maximum per size.
Because the nut only holds if the sheet is softer than the nut and flows into the undercut when pressed. Steel clinch nuts are rated for sheet up to about HRB 80 (HB 150). Stainless sheet and hard aluminium tempers need the hardened stainless version of the nut, or a rivet nut instead.
No. It needs a press with flat, parallel anvils that squeeze the nut into the punched hole; hammering deforms the thread and does not displace the sheet evenly. Hand arbor presses work for small sizes.
Yes. Standoffs, studs and nuts past the standard lengths or threads are turned from bar with the same clinch shank and undercut, so the standard installation tooling still fits, from 1 piece.
EKINSUN is a custom parts manufacturer that machines self-clinching nuts, studs and standoffs to drawing in steel, 303 / 304 / 316L stainless and aluminium, in metric, UNC and UNF threads, from 1 piece, with a quote within 12 hours.
There is no list price; the drivers are material, length, whether the end is blind, and quantity. A batch of 303 standoffs a few millimetres longer than standard is close to catalogue money; a single 316L stud with a shoulder is a turned part and priced as one. The quote states which.
Send the sheet, the thread and the length
Sheet material and thickness, thread and pitch, standoff or stud length, blind or through, hole size if punched, quantity. From 1 piece, quote within 12 hours.