A gearbox is down, the part is obsolete, and the original maker no longer supplies it? EKINSUN machines the replacement — gears, shafts, keys and housings — to your drawing or reverse-engineered from the worn part itself. No drawing or manufacturer reference needed. Quote in 12 hours.
A Replacement Gearbox Part — Even With No Drawing
Most people who search for a "custom gearbox manufacturer" don't need a brand-new gear train designed — they need one part remade so an otherwise-good machine runs again. That is exactly what we do. Send the failed component and, where possible, its mating part. We measure it, recover the geometry, and machine a correct replacement. For a gear we don't trace the worn teeth — we derive the gear from its numbers (tooth count, module, pressure angle), so even a chipped sample produces a part that meshes.
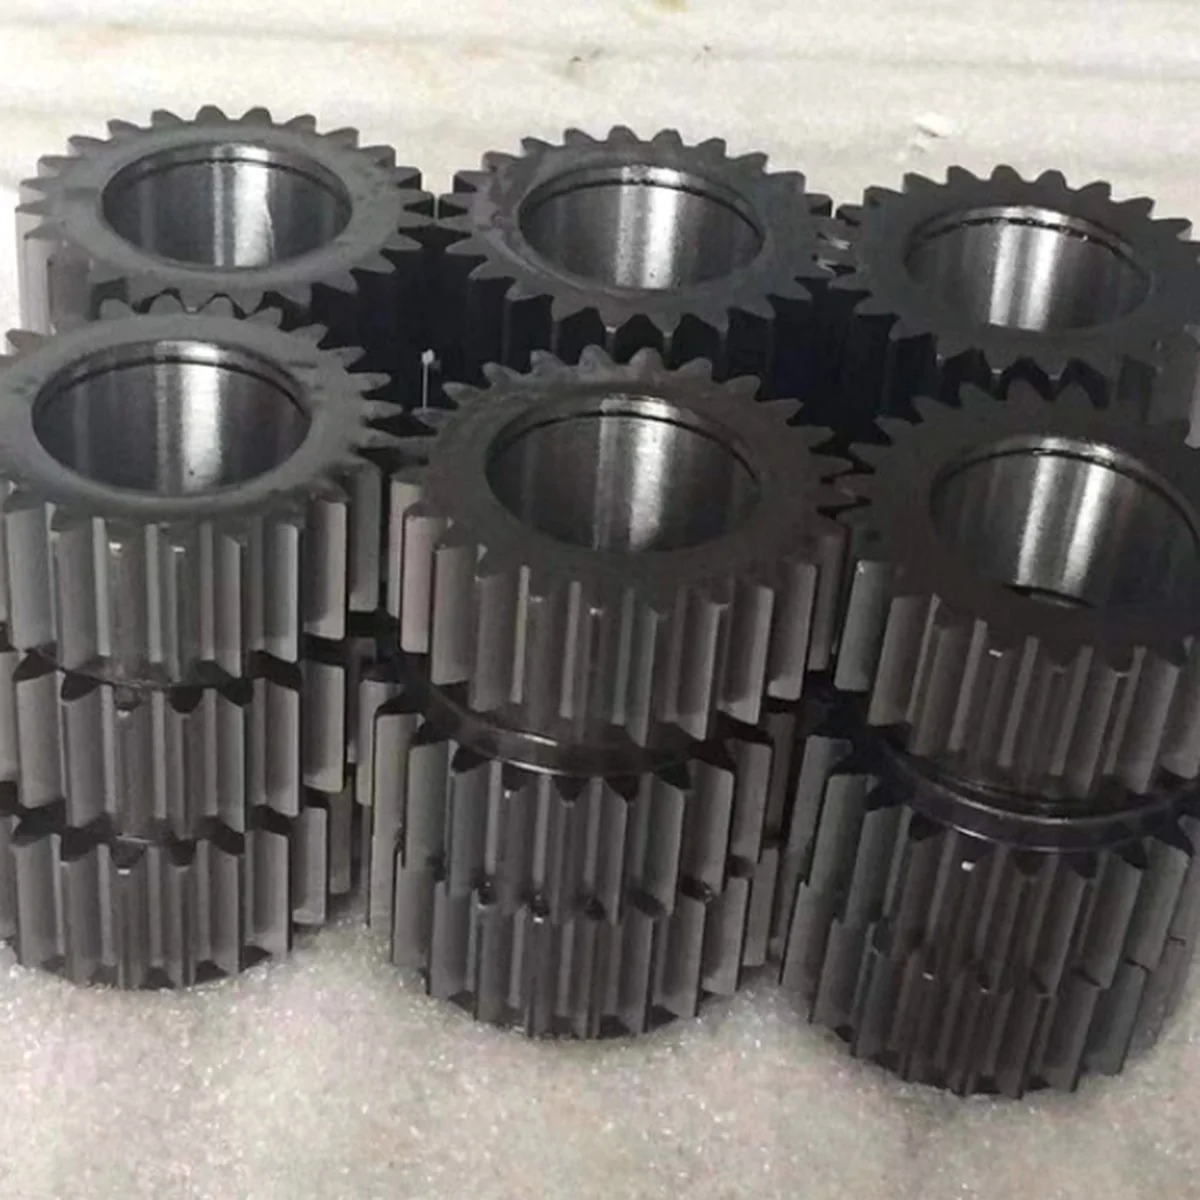
Gearbox Parts We Manufacture
| Part | What we make | Typical material |
|---|---|---|
| Spur & helical gears | Module ~0.5–8, any tooth count, bore & keyway to DIN 6885 / ANSI B17.1 to fit | 4140 / 8620 case-hardened steel |
| Bevel & worm gears | Worm and worm wheel sets, straight bevels | Steel worm + bronze wheel |
| Gear & output shafts | Splined, keyed, stepped — turned and ground | 4140 / 4340 steel |
| Pinions & cluster gears | High-ratio pinions, multi-gear blanks | Case-hardened alloy steel |
| Housings & covers | Milled housings, bearing bores, end covers | Aluminium or cast-iron equivalent |
| Keys, spacers, bushings | Drive keys, spacers, bronze bushings to size | Steel, bronze |
Honest scope: we manufacture the machined components of a gearbox and reverse-engineer discontinued ones. Bought-in items like bearings and seals are standard catalog parts — you source them, or we include them on request. We reproduce and upgrade existing gear trains; we don't design new ratios from scratch.
Reverse-Engineer an Obsolete Gearbox Part
This is the heart of the job. A gear's geometry is defined by a handful of standard parameters, so a worn or broken sample still yields a perfect new part — see how we derive a tooth form on our custom spur gear and custom worm gear pages. Shafts, keys and housings are measured directly. The full process is on our reverse engineering page, and the steel spur gear batch case shows it in practice. If your part is simply discontinued, our guide to replacing a discontinued gear walks through what we need.
Material & Hardening — Make It Last Longer
For power transmission we machine gears in 4140 or 8620 steel and harden them so the new part matches — or outlasts — the original. Surface hardening (case-hardening or nitriding) can raise allowable contact stress roughly 2–3× over a through-hardened gear, so a forced rebuild is a chance to upgrade a part that kept failing. Worm wheels are cut in bronze against a hardened steel worm; light-duty drives can use bronze or even Delrin. Where the drive has to run quietly and without grease, the wheel is cut in cast nylon or POM instead — see plastic gears and racks for the module range and the extra backlash a nylon gear needs, because it grows about 0.5 % damp and 2 % soaked. Tooth form, bore and shaft fits are verified on inspection.
Repair vs. Replace — Why a Remade Part Wins
When a single gear or shaft fails inside an otherwise sound gearbox, buying a whole new unit (if it even exists) is the expensive path. Remaking the failed component — often upgraded in material and hardness — gets the machine running for a fraction of the cost and keeps the rest of the proven assembly in service. For discontinued units it is frequently the only path.
Gearboxes We Supply Parts For
- Industrial reducers — worm and helical gear units on conveyors, mixers, pumps
- Machine-tool gearboxes — lathe and mill head/feed gears
- Automotive & motorsport — classic and discontinued transmission gears and shafts
- Marine, agricultural & material handling — drives where the OEM no longer supports the unit
Reading the Specification Off a Broken Gear
A gearbox gear defines itself, even with teeth missing. Three measurements recover the whole specification, and none of them needs the damaged flanks:
| Measure | How | What it gives |
|---|---|---|
| Outside diameter | Caliper over the tips, on an undamaged arc | With the tooth count: module m = OD ÷ (z + 2). A 66 mm gear with 20 teeth is module 3, exactly. |
| Tooth count z | Count them — broken teeth still leave their roots | Locks the module; with the mating gear’s count, confirms the centre distance |
| Centre distance a | Between bearing bores in the housing, not between worn shafts | Cross-check: for spur pairs a = m × (z₁ + z₂) ÷ 2. If it disagrees with the module from the OD, the gears are profile-shifted or helical — worth knowing before anything is cut. |
If the result lands on module 2.75 or another value no catalogue lists, that is not a measuring error — gearbox makers routinely used non-preferred modules and profile shift precisely so that spares would only fit their boxes. It is also why a catalogue gear of the “nearest” module does not mesh: module is not a dimension you can round. A 5 % module error concentrates contact at the tip and the new gear eats the old pinion in weeks.
Helical gears add one number: the helix angle, read with a protractor off a tooth trace on paper, or recovered from the axial lead. Bevel sets we take on as straight-tooth only — spiral bevels are Gleason territory and we say so rather than machine an approximation.
Gear Module Chart — Tooth Dimensions for Module 0.5 to 8
Every spur or helical gear cut to the ISO 53 basic rack has the same proportions: addendum ha = m, dedendum hf = 1.25 m, whole depth h = 2.25 m and circular pitch p = π m. Choose the module and the tooth is fixed; the tip diameter of an unshifted spur gear follows as da = m (z + 2). A module 2 gear therefore has 4.5 mm deep teeth on a 6.283 mm pitch, and with 20 teeth measures 44.0 mm over the tips.
| Module m | Circular pitch p = πm | Addendum ha = m | Dedendum hf = 1.25 m | Whole depth h = 2.25 m | Tip Ø da, z = 20 | Tip Ø da, z = 40 |
|---|---|---|---|---|---|---|
| m = 0.5 | 1.571 | 0.5 | 0.625 | 1.125 | 11 | 21 |
| m = 0.75 | 2.356 | 0.75 | 0.938 | 1.688 | 16.5 | 31.5 |
| m = 1 | 3.142 | 1 | 1.25 | 2.25 | 22 | 42 |
| m = 1.25 | 3.927 | 1.25 | 1.562 | 2.812 | 27.5 | 52.5 |
| m = 1.5 | 4.712 | 1.5 | 1.875 | 3.375 | 33 | 63 |
| m = 2 | 6.283 | 2 | 2.5 | 4.5 | 44 | 84 |
| m = 2.5 | 7.854 | 2.5 | 3.125 | 5.625 | 55 | 105 |
| m = 3 | 9.425 | 3 | 3.75 | 6.75 | 66 | 126 |
| m = 4 | 12.566 | 4 | 5 | 9 | 88 | 168 |
| m = 5 | 15.708 | 5 | 6.25 | 11.25 | 110 | 210 |
| m = 6 | 18.850 | 6 | 7.5 | 13.5 | 132 | 252 |
| m = 8 | 25.133 | 8 | 10 | 18 | 176 | 336 |
To recover the module from a broken gear, measure the tip diameter and count the teeth: m = da / (z + 2). A 20-tooth gear measuring 44.0 mm over the tips is module 2; one measuring 43.8 mm is still module 2 with worn or profile-shifted teeth — the remake is cut to the housing centre distance and the mating gear, not to the worn part. The bore is finished to H7 with a keyway from the DIN 6885 chart, and where the original was a plain spur gear custom spur gears in steel, stainless or brass from a sample are the usual route; helical, bevel and internal gears follow the same module rule with their own correction factors.
Material and Heat Treatment — What the Original Maker Chose, and Why
| Route | Typical steel | Result | Distortion | Where it belongs |
|---|---|---|---|---|
| Through-hardened / toughened | 42CrMo4 quenched and tempered, 28–34 HRC | One hardness through the section | None after machining — the bar arrives treated | Low-speed gears, one-off replacements, anything under about 6 m/s pitch-line speed |
| Case-hardened | 16MnCr5 / 20MnCr5, carburised | 58–62 HRC skin on a tough core, case 0.6–1.2 mm | Real — teeth move in the quench; ground afterwards on precision sets | What most OEM gearbox gears are; highest load capacity per size |
| Nitrided | 31CrMoV9 | ≈60 HRC skin, 0.1–0.4 mm deep | Minimal — done below tempering temperature, teeth cut finished | Gears that cannot be ground after hardening; fine-pitch work |
The honest consequence for a one-off replacement: a case-hardened original can often be replaced with through-hardened 42CrMo4 cut as a finished gear, because the replacement does not need to survive twenty years — it needs to run until the next overhaul, without the cost of carburising and post-grinding a single piece. Where the original ran against a hardened pinion at full load, we say so and quote the carburised route instead. The choice is stated on the quote, not hidden in it.
Where the other materials belong: aluminium has no place in a loaded gear — 6061 and 7075 are for the housing, the covers and the spacers around the gear train, not for teeth. Stainless gears exist for washdown and food-line boxes: 1.4301 (304) cut as a finished gear, accepted with the stated caveat that it galls against itself and carries less load than a hardened steel of the same size — where the duty allows it, it is quoted; where it does not, we say so.
Why a Welded-Up Tooth Fails Again
Weld repair of a broken tooth looks economical and usually is not, for one metallurgical reason: the weld itself can be made hard, but the heat-affected zone beside it falls to roughly 20–30 HRC — softer than the parent tooth — and that soft band sits exactly at the root fillet where the bending stress is highest. The repaired tooth fails at the toe of the weld, typically taking a neighbour with it. A remade gear costs more than a weld and less than the same weld done twice plus the second strip-down. Build-up welding has its place on shaft journals and housings, where the load is compressive and the geometry is restored by turning — we quote it there and decline it on teeth.
Where the Catalogue Stops on Gearbox Parts
| What the job needs | In the catalogue? | What happens then |
|---|---|---|
| Standard module, standard bore, metric spur gear | Yes — KHK, Mädler and others | Buy it and have the bore, keyway or web modified if needed — cheaper than cutting from bar |
| Non-preferred module (2.25, 2.75) or profile-shifted teeth | No | Cut to the measured geometry — this is most obsolete-gearbox work |
| Gear and shaft as one piece (pinion shaft) | No | Turned and cut from one bar, no keyway to work loose |
| Mating pair where both parts are worn | No | Cut as a set from the housing centre distance, checked in mesh |
| Bronze worm wheel to a surviving steel worm | No | See the worm gear page — the wheel must be hobbed to that worm’s diameter |
| Spiral bevel set | Specialist only | We decline — Gleason-type geometry needs dedicated machines |
| One piece, machine stopped | Not as a special | One piece is the normal order here; that is what this page is for |
See also cast parts made to order for gearbox housings, covers and bearing caps in grey or ductile iron.
Frequently Asked Questions
Yes — our most common gearbox job. Send the worn or broken part and its mate if possible. We recover the geometry — for a gear we derive tooth count, module and pressure angle — and machine a new part that fits. No drawing or manufacturer reference needed.
We manufacture the machined components — gears, shafts, keys, spacers and housings — and can reverse-engineer every machined part of a discontinued unit. Bearings and seals are catalog items you source or that we include on request. We reproduce and upgrade existing gear trains rather than designing new ratios.
Usually 4140/8620 steel (case-hardened), 4340 for high load, bronze for worm wheels and light-duty gears. We match the original or upgrade it — surface hardening can raise contact-stress capacity 2–3×.
Yes, MOQ 1 piece — a single gear or shaft to get a machine running, or a batch of spares. No minimum order.
Industrial reducers, machine-tool gearboxes, automotive and motorsport transmissions, marine, agricultural and material-handling drives. If a gear, shaft or housing can be turned, milled or hobbed, we can reproduce it.
Quote a Gearbox Part
Worn part, drawing or specs — all accepted. Reply in 12h.
// Qty & price
1 pc
Get it running
Single replacement part
10–50
Unit price drops
Spares on the shelf
100+
Best price
All tiers quoted upfront
- →No distributor — you pay the maker directly
- →CAD saved after first order — reorder spares anytime