Replacing a bearing and the locknut is seized, lost or a size nobody stocks? Rebuilding a machine spindle whose adjusting nut is long obsolete? Send the old nut or the shaft thread for a quote in 12 hours — we single-point the thread to match.
When the Standard Locknut Doesn't Exist
Bearing lock nuts and spindle nuts live by the catalogue — until the catalogue runs out. The KM and AN series cover the common bearing bores, but step outside them and the part vanishes: a shaft thread finer or coarser than the series pitch, a diameter above the largest KM, a machine-tool spindle nut the OEM stopped making decades ago, a left-hand adjusting nut, or a nut that needs extra height for more thread engagement. Standard shelves don't carry it, and no tap or die exists for the odd pitch.
EKINSUN machines it. We make custom bearing lock nuts and spindle nuts — round slotted (hook-spanner) nuts, precision set-screw and wedge locknuts, adjusting and retaining nuts — single-pointed to your exact thread and pitch, in the diameter, height and slot pattern you need. Reproduced from your old nut or the shaft it threads onto, no CAD file or part number required, one piece or a batch, quoted within 12 hours.
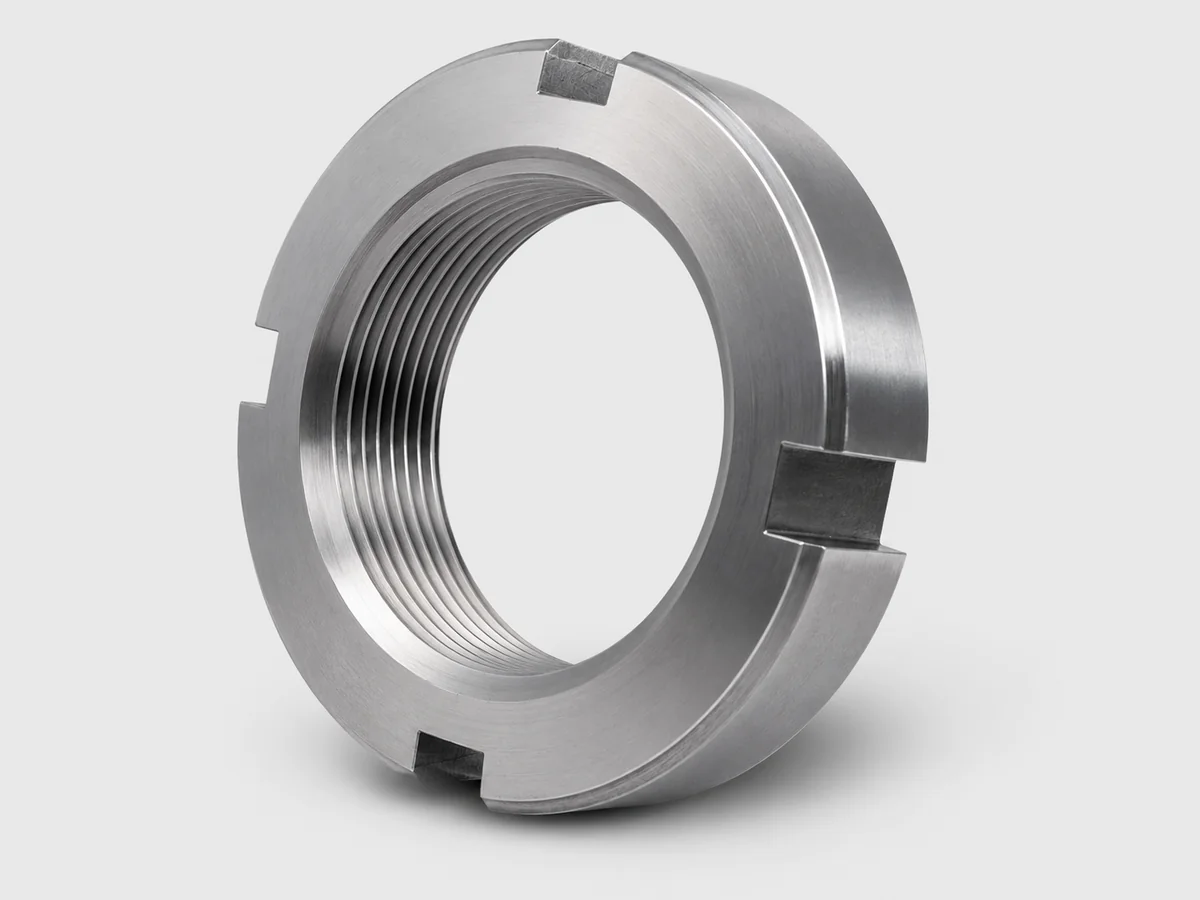
Nuts We Machine
Bearing lock nut (KM/AN)
Round slotted hook-spanner nut for bearing retention — any KM/AN size or beyond.
Spindle nut
Machine-tool spindle adjusting and retaining nuts, obsolete or non-standard.
Round slotted nut (DIN 1804)
Hook or face-spanner nut for bearings, pulleys and shaft ends.
Precision locknut
Set-screw, nylon-insert or wedge-segment locking for zero-backlash preload.
Oversized / tall nut
Extra height or wall for more thread engagement and higher preload.
Left-hand & special pitch
LH thread, extra-fine or odd pitch, single-pointed to match the shaft.
Series & Standards We Match
You don't need to identify the series — send the nut or shaft and we measure it. If you know the standard, here is what we reproduce:
| Series / Standard | What it is | What we match |
|---|---|---|
| KM (DIN 981) | Metric round slotted bearing locknut, KM0–KM40 and beyond | Metric fine thread, OD, height, slot count & width |
| AN (inch) | Imperial bearing locknut series (N-00 up) | Inch thread, slot pattern, tab-washer keyway |
| DIN 1804 | Slotted round nut / hook-spanner nut | Thread, face or side slots, spanner fit |
| MB / AN tab washer | Tongued lock washer that pairs with the nut | Bore tongue, OD tabs — supplied with the nut |
| Non-standard / OEM | Obsolete spindle nuts with no published spec | Reverse engineered from your old nut or shaft |
KM Series Thread Reference (typical)
| Size | Thread | Size | Thread |
|---|---|---|---|
| KM0 | M10 × 0.75 | KM5 | M25 × 1.5 |
| KM1 | M12 × 1 | KM6 | M30 × 1.5 |
| KM2 | M15 × 1 | KM7 | M35 × 1.5 |
| KM3 | M17 × 1 | KM8 | M40 × 1.5 |
| KM4 | M20 × 1 | KM9+ | M45 × 1.5 and up |
Need a thread between series sizes, a left-hand version, or a size above KM40? That's exactly what we machine — the reference above is only where the standard shelf stops.
KM lock nut dimensions above M90 (DIN 981)
The catalogue thins out exactly where the shafts get big. DIN 981 carries the KM series to M165, always in the one pitch the standard allows — 2 mm up to M150, 3 mm above — and skips two numbers on the way (there is no KM29 and no KM33). If your size and pitch are in the table, buy it from stock — no one-off can match that price, and we will say so. The rows are the standard values; the column that matters when you cannot buy one is the pitch, because a shaft cut M100×3 or M120×4 has no KM nut in any catalogue.
| KM | Thread d | Outside ø d2 | Slot-bottom ø d3 | Height h | Slot width b | Slot depth t | Tab washer |
|---|---|---|---|---|---|---|---|
| KM18 | M90×2 | 120 | 108 | 16 | 10 | 4 | MB18 |
| KM19 | M95×2 | 125 | 113 | 17 | 10 | 4 | MB19 |
| KM20 | M100×2 | 130 | 120 | 18 | 10 | 4 | MB20 |
| KM21 | M105×2 | 140 | 126 | 18 | 12 | 5 | MB21 |
| KM22 | M110×2 | 145 | 133 | 19 | 12 | 5 | MB22 |
| KM23 | M115×2 | 150 | 137 | 19 | 12 | 5 | MB23 |
| KM24 | M120×2 | 155 | 138 | 20 | 12 | 5 | MB24 |
| KM25 | M125×2 | 160 | 148 | 21 | 12 | 5 | MB25 |
| KM26 | M130×2 | 165 | 149 | 21 | 12 | 5 | MB26 |
| KM27 | M135×2 | 175 | 160 | 22 | 14 | 6 | MB27 |
| KM28 | M140×2 | 180 | 160 | 22 | 14 | 6 | MB28 |
| KM30 | M150×2 | 195 | 171 | 24 | 14 | 6 | MB30 |
| KM31 | M155×3 | 200 | 182 | 25 | 16 | 7 | MB31 |
| KM32 | M160×3 | 210 | 182 | 25 | 16 | 7 | MB32 |
| KM34 | M165×3 | 210 | 193 | 26 | 16 | 7 | MB33 |
Values per DIN 981, cross-checked between two published tables (Schrauben-Lexikon and Wegertseder, 2026). ISO 2982-2 continues the series to KM40 (M200×3) with the same construction. When the shaft thread is not the DIN pitch, when the housing needs a lower height than h, or when you need more or fewer than four slots for the tab washer you already have, that is the nut we machine — send the shaft thread and the washer, and we turn the nut to match.
| What you need | In the catalogue? | What we machine |
|---|---|---|
| A KM nut in a DIN 981 size, M10×0.75 to M165×3 | Yes — bearing distributors stock the series | Buy it from stock; we will tell you so in the quote. |
| A shaft cut to a pitch DIN 981 does not carry — M100×3, M120×4, or left-hand | No — the standard fixes one pitch per size | Nut single-pointed to the shaft’s actual thread, four slots to your MB washer. |
| Lower height than h, or a different slot count for a washer you already have | No | Turned to the height the housing allows, slots milled to the count and width you state. |
| A metric shaft with an imperial AN-series washer, or the reverse | No — the two series do not cross | Nut cut to the shaft, slots cut to the washer, one piece up. |
Measure before you order. Ten pitches of a DIN 981 shaft thread measure 20 mm up to M150 and 30 mm above. Lay a rule across ten crests of your shaft: if it reads 20 on an M100, buy the KM 20 from stock; if it reads 30 or 40, the shaft was cut outside the KM series and no catalogue lock nut will run on it — send the diameter, the pitch and the washer you have, and we turn the nut to match. How to read the pitch off a large thread →
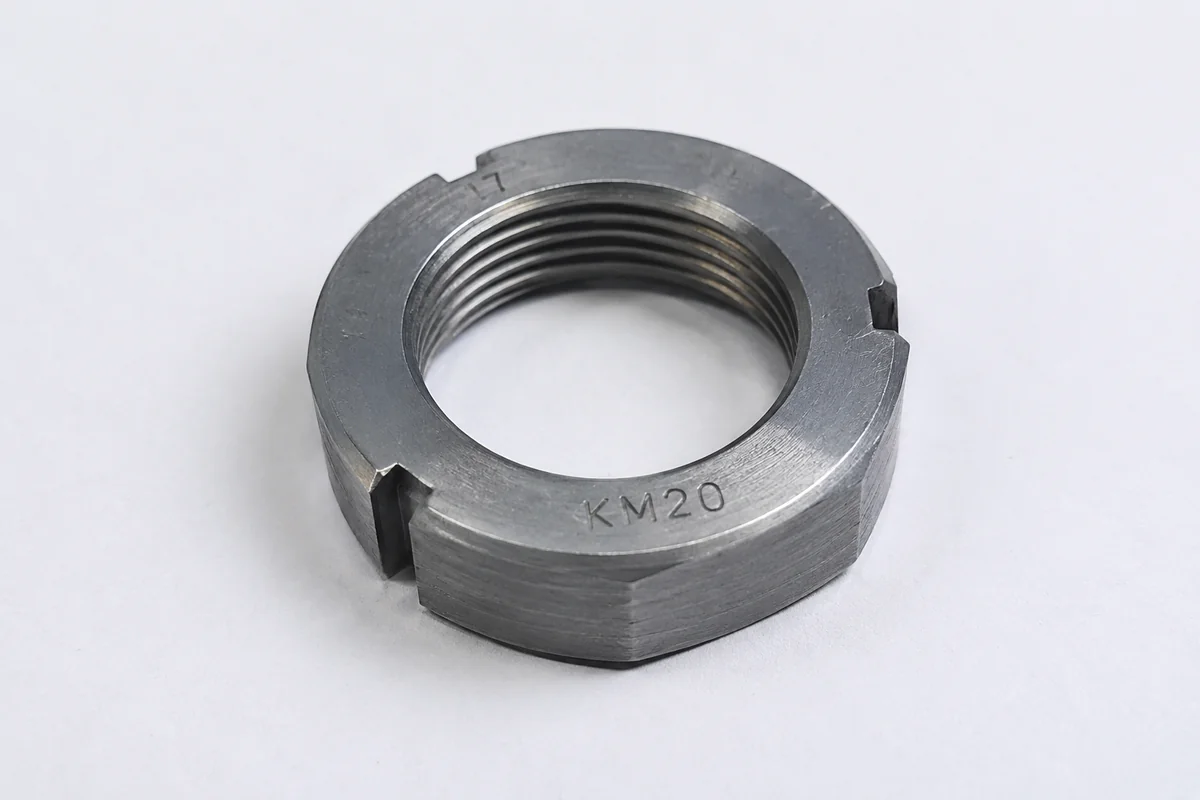
Materials
| Material | Best for | Notes |
|---|---|---|
| Medium-carbon / alloy steel | Standard bearing & spindle nuts | Strength and thread-wear resistance; can be plated or blackened |
| 304 stainless | Washdown, food, humid or outdoor service | General corrosion resistance |
| 316 stainless | Marine and chemical service | Chloride resistance for seawater and coastal plant |
| Brass | Where a softer nut must protect the shaft thread | Non-galling, good for adjustment nuts |
| 6061 / 7075 aluminium | Lightweight spindles — motorsport, aerospace | 7075 where preload load is high and weight still matters |
The nut is only as good as how it stays put. A bearing locknut that backs off under vibration destroys the bearing it was holding. We machine the locking feature to your design — the tongue slot for an MB / AN tab washer, radial set screws, a nylon insert, or a wedge segment for a true zero-backlash precision locknut — and supply the matching washer in the same order so the assembly locks the way the original did.
How It Works
Send the old nut or the shaft
The seized, worn or lost nut — or the shaft thread it fits. Tell us the locking method (tab washer, set screw, wedge) if you know it.
We measure and rebuild the thread
Thread, pitch, hand, OD, height and slots measured and drawn — free of charge, no part number needed. See how we work from a sample.
You approve, we machine
Single-pointed thread, slots cut, locking feature machined in, matching tab washer made — inspected before shipping.
Reorder anytime
We keep the thread and slot data on file, so the next bearing service is a one-line email at a lower unit price.
Who Orders Custom Lock Nuts
"The bearing came with a locknut in a size I can't source, and the machine's down"
Send the old nut or the shaft. We reproduce the KM/AN nut and its tab washer to fit, in days — so the bearing job isn't held up by a locknut nobody stocks in that thread.
"This spindle's adjusting nut is obsolete and I need the preload exactly right"
We copy the obsolete nut — thread, slots and locking — and can add height for more engagement or a wedge lock for zero backlash, so the rebuilt spindle holds preload like new.
"My design uses a non-standard fine pitch and there's no catalogue nut for it"
We single-point the nut to your pitch — left-hand, extra-fine, whatever the shaft needs — with your slot pattern and locking feature, repeatable from saved data with material certs.
"I need the same locknut but lighter, and in the exact thread on my shaft"
We machine it in 6061 or 7075 aluminium to the exact thread and preload feature — light, precise, and made one-off if that's all you need.
What Buyers Search For
Will it fit? KM lock nut checks before you order
KM nuts come in one thread each: KM4 is M20×1, KM5 is M25×1.5, KM7 is M35×1.5. A spindle cut M20×1.5 takes no KM nut at all — the M20×1 nut starts, binds and stops. Above M150 the DIN 981 series changes to a 3 mm pitch, and two numbers do not exist (there is no KM29 and no KM33). If the shaft thread is between series sizes, left-hand, or at a pitch the table does not show, the nut is machined, and it is cut to the shaft you measure, not to a catalogue.
What do I need to lock a bearing on a shaft with a non-standard thread?
A lock nut cut to the shaft's thread, and an MB-style tab washer at the same bore, so the tab still locates in the shaft keyway. Send the thread readings — outside diameter, pitch over ten turns, hand — or the old nut, and both parts are drawn as a pair.
Same lock nut, but left-hand, taller, or in 316
A left-hand version for a shaft that runs the other way, an extra-tall body for more thread engagement, a slot count to suit your hook spanner, or stainless for a washdown machine — each is a variant of the same drawing, one piece and up, quoted in 12 hours.
A shaft thread that no nut series covers at all, such as M27×1.75, gets the same treatment: see the M27×1.75 nut page for hex, thin, coupling and slotted forms at that pitch.
Frequently Asked Questions
Yes — that is the usual reason to have one machined. The KM/AN series stops at set sizes and pitches; when your shaft thread falls outside it, or you need a diameter or height the catalogue doesn't list, we machine the round slotted nut to your exact thread, OD, height and slot pattern so a standard hook spanner still fits.
Yes. Send the old nut — even seized or partly stripped — or the shaft it threads onto, and we measure the thread, pitch, slots and locking feature and reproduce it. No part number or drawing needed; we work from the physical part.
No. Left-hand, extra-fine, and non-standard pitches are routine on machine spindles and adjusting nuts. Tell us the pitch and hand, or send the shaft, and we single-point the thread to match — including odd pitches no tap or die exists for.
Yes. We make the matching MB / AN tab washer, tongued or slotted, in the same order so the assembly locks the way it should. If your design uses set screws, a nylon insert or a wedge segment instead, we machine that locking feature into the nut itself.
Standard is medium-carbon or alloy steel for strength and thread wear; 303/304/316 stainless for corrosive, washdown or marine service; brass where a softer nut protects the shaft. For lightweight spindles — motorsport and aerospace — we machine them in 6061-T6 or 7075-T6 aluminium. All cut from solid with EN 10204 3.1 certificates on request.
Yes — and for the plain hex family see large & oversize custom nuts (M30–M160). Extra height for more thread engagement, a larger OD for spanner clearance, deeper or extra slots, or a heavier wall for high preload — all machined to your requirement. Tell us the load or preload and we advise on height and material.
Related Custom Fasteners
Bearing and spindle nuts often ship with their neighbours. We also machine castle & slotted nuts to DIN 935, coupling nuts including reducing and LH/RH, and any non-standard thread bolts to match. For the shaft side of a bearing rebuild see pump replacement parts, and if the bearing itself is obsolete we can reverse engineer a bearing from a worn part. For anything one-off, special fasteners made to drawing.
Lock Nut Quote
Send the old nut or the shaft thread. Reply in 12h.
// Qty & price
1 pc
Sample price
Confirm fit before a run
10–50
Unit price drops
Setup cost shared
100+
Best price
All tiers quoted upfront
- →No distributor — you pay the maker directly
- →Thread & slot data saved — reorder anytime at lower unit price