Metric Thread Pitch Chart — Coarse and Fine Pitch, M1 to M64
Every metric size has one coarse pitch (ISO 261) and one or two fine pitches that bolts and nuts are made in (the ISO 262 selection); M10, for example, is 1.5 mm coarse and 1.25 mm or 1 mm fine. M7 has a standard thread but no standard hex bolt; bolts in M7, M9 and M11 are made to order (see odd metric bolt sizes). EKINSUN LTD is a custom parts manufacturer that cuts coarse, fine and inch threads to order and makes coarse-to-fine adapters, studs and nuts from 1 piece.
| Size | Coarse pitch | Ten coarse threads | Fine pitch(es) | Ten fine threads |
|---|---|---|---|---|
| M1 | 0.25 | 2.5 | 0.2 | 2 |
| M1.2 | 0.25 | 2.5 | 0.2 | 2 |
| M1.4 | 0.3 | 3 | 0.2 | 2 |
| M1.6 | 0.35 | 3.5 | 0.2 | 2 |
| M1.8 | 0.35 | 3.5 | 0.2 | 2 |
| M2 | 0.4 | 4 | 0.25 | 2.5 |
| M2.5 | 0.45 | 4.5 | 0.35 | 3.5 |
| M3 | 0.5 | 5 | 0.35 | 3.5 |
| M3.5 | 0.6 | 6 | 0.35 | 3.5 |
| M4 | 0.7 | 7 | 0.5 | 5 |
| M5 | 0.8 | 8 | 0.5 | 5 |
| M6 | 1 | 10 | 0.75 | 7.5 |
| M7 | 1 | 10 | 0.75 | 7.5 |
| M8 | 1.25 | 12.5 | 1 / 0.75 | 10 / 7.5 |
| M10 | 1.5 | 15 | 1.25 / 1 | 12.5 / 10 |
| M12 | 1.75 | 17.5 | 1.5 / 1.25 | 15 / 12.5 |
| M14 | 2 | 20 | 1.5 | 15 |
| M16 | 2 | 20 | 1.5 | 15 |
| M18 | 2.5 | 25 | 2 / 1.5 | 20 / 15 |
| M20 | 2.5 | 25 | 2 / 1.5 | 20 / 15 |
| M22 | 2.5 | 25 | 2 / 1.5 | 20 / 15 |
| M24 | 3 | 30 | 2 | 20 |
| M27 | 3 | 30 | 2 | 20 |
| M30 | 3.5 | 35 | 2 | 20 |
| M33 | 3.5 | 35 | 2 | 20 |
| M36 | 4 | 40 | 3 | 30 |
| M39 | 4 | 40 | 3 | 30 |
| M42 | 4.5 | 45 | 3 | 30 |
| M45 | 4.5 | 45 | 3 | 30 |
| M48 | 5 | 50 | 3 | 30 |
| M52 | 5 | 50 | 4 | 40 |
| M56 | 5.5 | 55 | 4 | 40 |
| M60 | 5.5 | 55 | 4 | 40 |
| M64 | 6 | 60 | 4 | 40 |
Coarse pitch per ISO 261; fine pitches per the ISO 262 selection. ISO 261 defines more fine pitches than the ones listed, for example M10 × 0.75, M12 × 1 and M16 × 1; we cut those as well. A size written without a pitch, such as M12 × 40, is coarse. Tap drill sizes for coarse and fine threads are on the clearance hole and tap drill chart; pitches above M64 on fine pitch above M64; standard bolt lengths for each size on the bolt length chart.
Buying bolts, nuts or adapters in these threads? Standard coarse and fine bolts, nuts and studs can also be supplied from stock; fine pitches in A4 stainless, pitches outside the ISO 262 selection and coarse-to-fine adapters are made to order from 1 piece. The more pieces you order, the lower the unit price. Send the thread, the length, the material and the quantity; quote in 12 hours.
Inch Thread Pitch Chart — UNC, UNF and UNEF
Inch threads are counted in threads per inch (TPI): UNC is the coarse series, UNF the fine and UNEF the extra-fine, and the pitch in millimetres is 25.4 divided by the TPI. A 1/4 in bolt is 1/4-20 UNC or 1/4-28 UNF; sizes below 1/4 in are numbered from #0 to #12.
| Size | Major Ø in / mm | UNC TPI (pitch / ten threads) | UNF TPI (pitch / ten threads) | UNEF TPI (pitch / ten threads) |
|---|---|---|---|---|
| #0 | 0.0600 / 1.524 | — | 80 (0.318 / 3.18) | — |
| #1 | 0.0730 / 1.854 | 64 (0.397 / 3.97) | 72 (0.353 / 3.53) | — |
| #2 | 0.0860 / 2.184 | 56 (0.454 / 4.54) | 64 (0.397 / 3.97) | — |
| #3 | 0.0990 / 2.515 | 48 (0.529 / 5.29) | 56 (0.454 / 4.54) | — |
| #4 | 0.1120 / 2.845 | 40 (0.635 / 6.35) | 48 (0.529 / 5.29) | — |
| #5 | 0.1250 / 3.175 | 40 (0.635 / 6.35) | 44 (0.577 / 5.77) | — |
| #6 | 0.1380 / 3.505 | 32 (0.794 / 7.94) | 40 (0.635 / 6.35) | — |
| #8 | 0.1640 / 4.166 | 32 (0.794 / 7.94) | 36 (0.706 / 7.06) | — |
| #10 | 0.1900 / 4.826 | 24 (1.058 / 10.58) | 32 (0.794 / 7.94) | — |
| #12 | 0.2160 / 5.486 | 24 (1.058 / 10.58) | 28 (0.907 / 9.07) | 32 (0.794 / 7.94) |
| 1/4 in | 0.2500 / 6.350 | 20 (1.270 / 12.70) | 28 (0.907 / 9.07) | 32 (0.794 / 7.94) |
| 5/16 in | 0.3125 / 7.938 | 18 (1.411 / 14.11) | 24 (1.058 / 10.58) | 32 (0.794 / 7.94) |
| 3/8 in | 0.3750 / 9.525 | 16 (1.588 / 15.88) | 24 (1.058 / 10.58) | 32 (0.794 / 7.94) |
| 7/16 in | 0.4375 / 11.112 | 14 (1.814 / 18.14) | 20 (1.270 / 12.70) | 28 (0.907 / 9.07) |
| 1/2 in | 0.5000 / 12.700 | 13 (1.954 / 19.54) | 20 (1.270 / 12.70) | 28 (0.907 / 9.07) |
| 9/16 in | 0.5625 / 14.287 | 12 (2.117 / 21.17) | 18 (1.411 / 14.11) | 24 (1.058 / 10.58) |
| 5/8 in | 0.6250 / 15.875 | 11 (2.309 / 23.09) | 18 (1.411 / 14.11) | 24 (1.058 / 10.58) |
| 3/4 in | 0.7500 / 19.050 | 10 (2.540 / 25.40) | 16 (1.588 / 15.88) | 20 (1.270 / 12.70) |
| 7/8 in | 0.8750 / 22.225 | 9 (2.822 / 28.22) | 14 (1.814 / 18.14) | 20 (1.270 / 12.70) |
| 1 in | 1.0000 / 25.400 | 8 (3.175 / 31.75) | 12 (2.117 / 21.17) | 20 (1.270 / 12.70) |
| 1-1/8 in | 1.1250 / 28.575 | 7 (3.629 / 36.29) | 12 (2.117 / 21.17) | — |
| 1-1/4 in | 1.2500 / 31.750 | 7 (3.629 / 36.29) | 12 (2.117 / 21.17) | — |
| 1-3/8 in | 1.3750 / 34.925 | 6 (4.233 / 42.33) | 12 (2.117 / 21.17) | — |
| 1-1/2 in | 1.5000 / 38.100 | 6 (4.233 / 42.33) | 12 (2.117 / 21.17) | — |
Threads per inch per ASME B1.1. #0 exists only as #0-80 UNF. Metric and inch threads that look alike (M6 and 1/4-20, M12 × 1.75 and 1/2-13) are compared on the metric vs imperial thread chart; British threads on the Whitworth thread chart. Hydraulic JIC, AN and ORB fittings use UNF and UN threads by dash size (-6 is 9/16-18, -8 is 3/4-16): see the JIC and ORB fitting size chart.
How to Measure Thread Pitch — Ten Threads Over a Rule
A caliper and a steel rule are enough to tell coarse from fine and metric from inch. Measure the outside diameter of the bolt with the caliper, then lay the rule along the thread and read the length of ten threads from crest to crest; ten threads divided by ten is the pitch. A diameter that is not a round number of millimetres points to an inch thread; for inch threads 254 divided by the ten-thread length gives the threads per inch. A thread gauge confirms the reading: the right leaf sits in the thread with no light between the teeth. Check the direction too: a left-hand thread rises to the left when the bolt is held upright.
| Outside Ø (mm) | Ten threads measure (mm) | Thread |
|---|---|---|
| about 10 | 15.0 | M10 coarse (M10 × 1.5) |
| about 10 | 12.5 or 10.0 | M10 fine (M10 × 1.25 or M10 × 1) |
| about 12 | 17.5 | M12 coarse (M12 × 1.75) |
| about 12 | 15.0 or 12.5 | M12 fine (M12 × 1.5 or M12 × 1.25) |
| about 6.3 | 12.70 | 1/4-20 UNC (inch) |
| about 6.3 | 9.07 | 1/4-28 UNF (inch) |
| about 12.7 | 19.54 or 12.70 | 1/2-13 UNC or 1/2-20 UNF (inch) |
| a round number | between two chart values | a special pitch, a Whitworth thread or a worn thread: measure again over twenty threads |
Coarse vs Fine Thread — Strength, Travel per Turn and Where Each Is Used
A fine thread of the same diameter has a larger tensile stress area, so in the same property class it carries more tensile load: M10 × 1 has 64.5 mm² against 58.0 mm² for M10 × 1.5. The stress area is calculated from the pitch and minor diameters as ISO 898-1 defines it; the values below reproduce the ones printed in the standard.
| Coarse thread | As coarse (mm²) | Fine thread: As (mm²) | Fine vs coarse |
|---|---|---|---|
| M8 × 1.25 | 36.6 | M8 × 1: 39.2 | +7 % |
| M10 × 1.5 | 58.0 | M10 × 1.25: 61.2; M10 × 1: 64.5 | +6 %; +11 % |
| M12 × 1.75 | 84.3 | M12 × 1.5: 88.1; M12 × 1.25: 92.1 | +5 %; +9 % |
| M16 × 2 | 157 | M16 × 1.5: 167 | +6 % |
| M20 × 2.5 | 245 | M20 × 2: 258; M20 × 1.5: 272 | +5 %; +11 % |
| M24 × 3 | 353 | M24 × 2: 384 | +9 % |
| M30 × 3.5 | 561 | M30 × 2: 621 | +11 % |
| M36 × 4 | 817 | M36 × 3: 865 | +6 % |
| Choose coarse when | Choose fine when |
|---|---|
| The thread is tapped into aluminium, cast iron or plastic: the deeper thread is less likely to strip | The wall is thin or the thread engagement is short, and more threads have to carry the load |
| Assembly speed matters: more travel per turn, and a coarse thread starts more easily by hand | An adjustment needs small steps: the pitch is the travel per turn, 1 mm on M10 × 1 against 1.5 mm on M10 × 1.5 |
| The part may be dirty, coated or reused many times | More tensile load has to go through the same diameter (see the stress area table) |
| Spare parts have to be easy to buy: most bolts and nuts on the shelf are coarse | The mating part already has a fine thread (vehicle, hydraulic and instrument parts) |
Coarse-to-Fine Thread Adapters — Same Diameter, Different Pitch
A coarse-to-fine thread adapter joins two threads of the same diameter and different pitch, such as M10 × 1.5 to M10 × 1.25 or 1/2-13 UNC to 1/2-20 UNF. It is used where a part with a fine thread has to take a standard coarse bolt or fitting, or the other way round, and neither part can be re-threaded. We make it as a male-female adapter, a female-female coupling or a male-male stud, with a hex or flats for a spanner, from 1 piece.
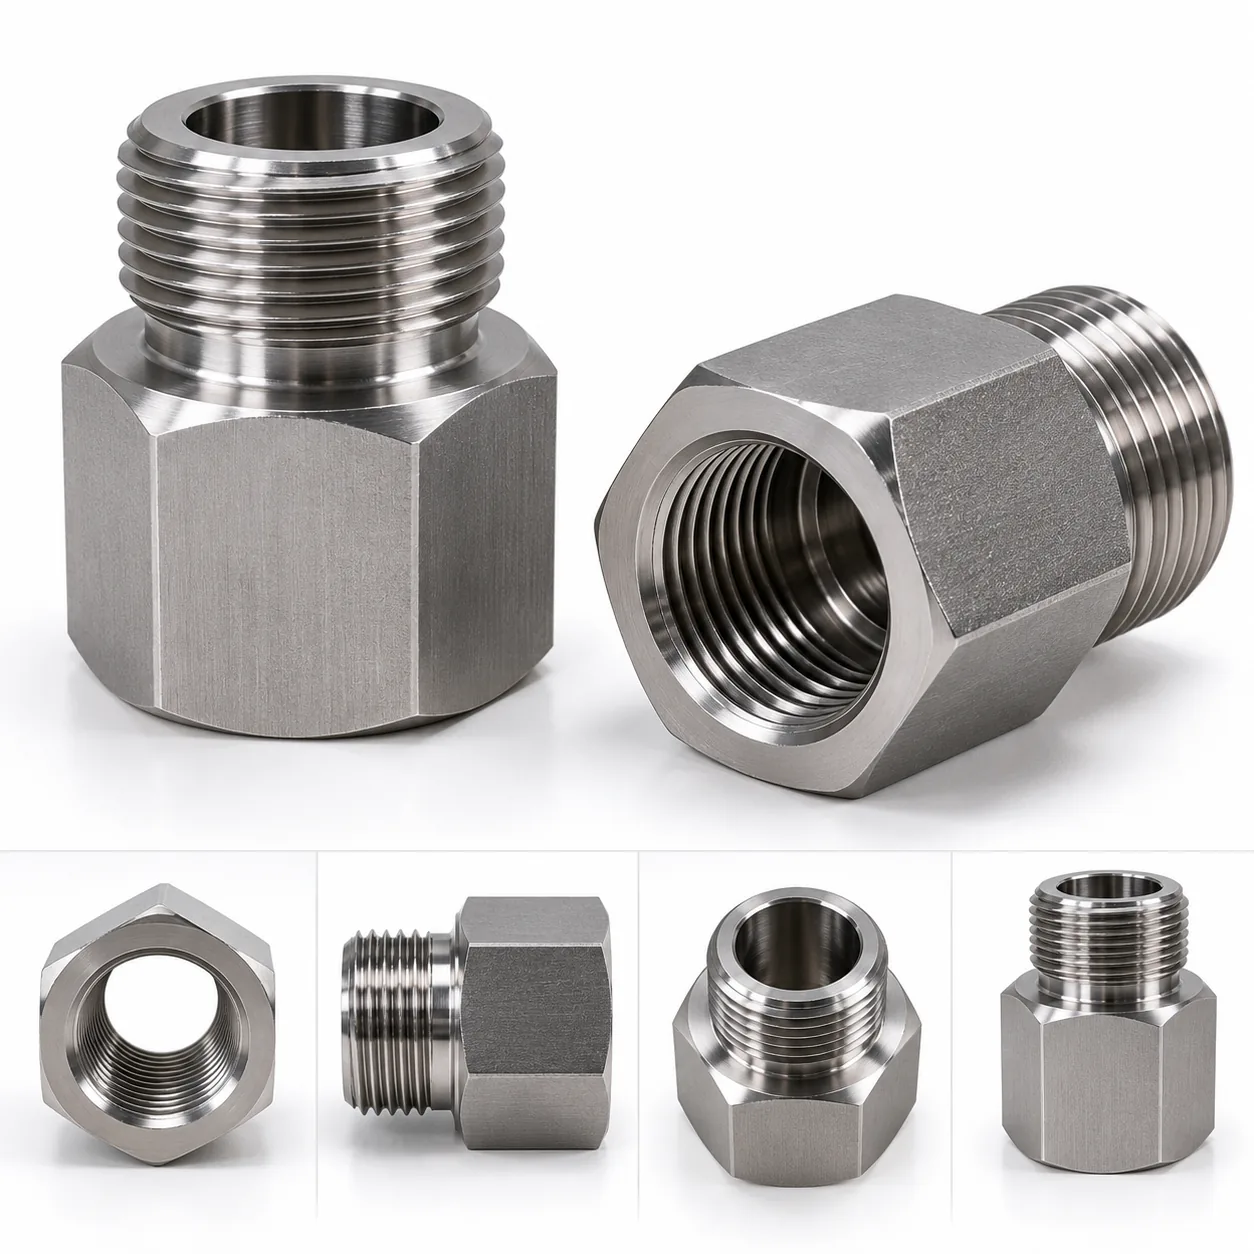
| Coarse thread | Fine thread | Ten threads coarse / fine (mm) |
|---|---|---|
| M6 × 1 | M6 × 0.75 | 10 / 7.5 |
| M8 × 1.25 | M8 × 1 | 12.5 / 10 |
| M10 × 1.5 | M10 × 1.25 | 15 / 12.5 |
| M10 × 1.5 | M10 × 1 | 15 / 10 |
| M12 × 1.75 | M12 × 1.5 | 17.5 / 15 |
| M12 × 1.75 | M12 × 1.25 | 17.5 / 12.5 |
| M14 × 2 | M14 × 1.5 | 20 / 15 |
| M16 × 2 | M16 × 1.5 | 20 / 15 |
| M18 × 2.5 | M18 × 1.5 | 25 / 15 |
| M20 × 2.5 | M20 × 1.5 | 25 / 15 |
| M22 × 2.5 | M22 × 1.5 | 25 / 15 |
| M24 × 3 | M24 × 2 | 30 / 20 |
| 1/4-20 UNC | 1/4-28 UNF | 12.70 / 9.07 |
| 5/16-18 UNC | 5/16-24 UNF | 14.11 / 10.58 |
| 3/8-16 UNC | 3/8-24 UNF | 15.88 / 10.58 |
| 7/16-14 UNC | 7/16-20 UNF | 18.14 / 12.70 |
| 1/2-13 UNC | 1/2-20 UNF | 19.54 / 12.70 |
| 9/16-12 UNC | 9/16-18 UNF | 21.17 / 14.11 |
| 5/8-11 UNC | 5/8-18 UNF | 23.09 / 14.11 |
| 3/4-10 UNC | 3/4-16 UNF | 25.40 / 15.88 |
| 7/8-9 UNC | 7/8-14 UNF | 28.22 / 18.14 |
| 1-8 UNC | 1-12 UNF | 31.75 / 21.17 |
Price for a coarse-to-fine adapter: tap its row above, or send both threads, male or female on each end, and the length. Made from 1 piece; the more pieces, the lower the unit price.
Materials: 304 (1.4301) or 316L (1.4404) stainless, brass CW614N, 42CrMo4 alloy steel for load-bearing studs, and 6061 aluminium for light-duty adapters such as instrument mounts. Adapters between two different diameters are on custom metric thread adapters and thread adapters; couplings with a different thread at each end on double-ended studs.
For a pitch the chart does not list, the basic-profile values are worked out from the same constants: the M27×1.75 thread dimensions page gives pitch diameter, minor diameters, tap drill and wire size for that special pitch.
On the Shelf or Made to Order
Standard coarse and fine bolts and nuts are shelf parts and cost less than any machined part. We supply standard sizes too, and for one piece needed today a local store is quicker. We make the threads and pairs the shelf does not carry, from 1 piece.
| What you need | On the shelf? | What we do |
|---|---|---|
| A bolt, nut or stud in a standard size and pitch — M6 × 1, M10 × 1.25, 1/4-20, 3/8-24 — in steel or A2 stainless | Yes — hardware and industrial supply stores | Buy it from stock — from us (standard sizes can be supplied from stock; the more pieces, the lower the unit price) or, for one piece today, at a local hardware or industrial supply store. |
| A fine-pitch nut or bolt in A4 (316) stainless, or a fine pitch above M24 | Partly | Made to order from 1 piece in 316L. |
| A coarse-to-fine adapter or coupling: M10 × 1.5 to M10 × 1.25, 1/2-13 to 1/2-20 | Rarely — a few sizes | Made in the pair you name, male-female, female-female or male-male, from 1 piece. |
| A pitch outside the ISO 262 selection: M10 × 0.75, M12 × 1, M16 × 1, M20 × 1 | No | Cut to the pitch you measure; every ISO 261 fine pitch is possible. |
| Metric on one end, inch on the other: M6 × 1 to 1/4-20, M12 × 1.5 to 1/2-20 | No | Made to order; see metric to imperial thread adapters. |
| An inch extra-fine or constant-pitch thread: 3/4-20 UNEF, 1-20 UNEF, 1-1/4-12 UN | Partly | Made with the thread you name. |
| A left-hand coarse or fine thread | Rarely | Cut left-hand in the same pitch; see non-standard thread bolts. |
Thread Pitch by Size — Quick Answers
What is the thread pitch of M3?
M3 has a coarse pitch of 0.5 mm, so ten threads measure 5 mm; its fine pitch is 0.35 mm (ten threads = 3.5 mm).
What is the thread pitch of M4?
M4 has a coarse pitch of 0.7 mm, so ten threads measure 7 mm; its fine pitch is 0.5 mm (ten threads = 5 mm).
What is the thread pitch of M5?
M5 has a coarse pitch of 0.8 mm, so ten threads measure 8 mm; its fine pitch is 0.5 mm (ten threads = 5 mm).
What is the thread pitch of M6?
M6 has a coarse pitch of 1 mm, so ten threads measure 10 mm; its fine pitch is 0.75 mm (ten threads = 7.5 mm).
What is the thread pitch of M8?
M8 has a coarse pitch of 1.25 mm, so ten threads measure 12.5 mm; its fine pitches are 1 mm (ten threads = 10 mm) and 0.75 mm (ten threads = 7.5 mm).
What is the thread pitch of M10?
M10 has a coarse pitch of 1.5 mm, so ten threads measure 15 mm; its fine pitches are 1.25 mm (ten threads = 12.5 mm) and 1 mm (ten threads = 10 mm).
What is the thread pitch of M12?
M12 has a coarse pitch of 1.75 mm, so ten threads measure 17.5 mm; its fine pitches are 1.5 mm (ten threads = 15 mm) and 1.25 mm (ten threads = 12.5 mm).
What is the thread pitch of M14?
M14 has a coarse pitch of 2 mm, so ten threads measure 20 mm; its fine pitch is 1.5 mm (ten threads = 15 mm).
What is the thread pitch of M16?
M16 has a coarse pitch of 2 mm, so ten threads measure 20 mm; its fine pitch is 1.5 mm (ten threads = 15 mm).
What is the thread pitch of M20?
M20 has a coarse pitch of 2.5 mm, so ten threads measure 25 mm; its fine pitches are 2 mm (ten threads = 20 mm) and 1.5 mm (ten threads = 15 mm).
What is the thread pitch of M24?
M24 has a coarse pitch of 3 mm, so ten threads measure 30 mm; its fine pitch is 2 mm (ten threads = 20 mm).
What is the thread pitch of M30?
M30 has a coarse pitch of 3.5 mm, so ten threads measure 35 mm; its fine pitch is 2 mm (ten threads = 20 mm).
What is the thread pitch of a 1/4 in bolt?
A 1/4 in bolt is 1/4-20 UNC coarse, a pitch of 1.270 mm (ten threads = 12.70 mm), or 1/4-28 UNF fine, 0.907 mm (ten threads = 9.07 mm), and the UNEF extra-fine thread is 1/4-32 (0.794 mm).
What is the thread pitch of a 3/8 in bolt?
A 3/8 in bolt is 3/8-16 UNC coarse, a pitch of 1.588 mm (ten threads = 15.88 mm), or 3/8-24 UNF fine, 1.058 mm (ten threads = 10.58 mm), and the UNEF extra-fine thread is 3/8-32 (0.794 mm).
What is the thread pitch of a 1/2 in bolt?
A 1/2 in bolt is 1/2-13 UNC coarse, a pitch of 1.954 mm (ten threads = 19.54 mm), or 1/2-20 UNF fine, 1.270 mm (ten threads = 12.70 mm), and the UNEF extra-fine thread is 1/2-28 (0.907 mm).
What to Send for a Quote
Both threads (size and pitch, or size and threads per inch), male or female on each end, the overall length and the length of each thread, the hex size if there is one, the material and the quantity. For a replacement, a photo of the part beside a rule and a ten-thread reading are enough. Made from 1 piece; quote in 12 hours.
How deep a thread has to go into an aluminium or a steel plate, 2 × d or 1 × d, is on plates with tapped holes.
Thread Pitch FAQ
An M8 bolt has a coarse pitch of 1.25 mm, so ten threads measure 12.5 mm. The fine pitches for M8 are 1 mm and 0.75 mm (ISO 262). A size written without a pitch, such as M8 × 30, is coarse.
The diameter is the same; a fine thread has a smaller pitch, so more threads fit in the same length. M10 is 1.5 mm coarse and 1.25 mm or 1 mm fine; a 1/4 in screw has 20 threads per inch coarse (UNC) and 28 fine (UNF). A coarse and a fine thread of the same diameter do not screw together.
In tension, a fine-thread bolt of the same diameter and property class carries more load, because its tensile stress area is larger: M10 × 1.25 has 61.2 mm² against 58.0 mm² for M10 coarse, about 6 % more, and M20 × 1.5 has 272 mm² against 245 mm², about 11 % more. In aluminium and cast iron coarse threads are the default, because the deeper thread is less likely to strip.
Lay a steel rule along the thread, measure across ten threads from crest to crest and divide by ten: 15 mm over ten threads is a 1.5 mm pitch. For an inch thread, count the threads in one inch, or divide 254 by the ten-thread length in millimetres: 12.7 mm gives 20 threads per inch. A reading that fits neither chart points to a special pitch, a Whitworth thread or a worn thread.
No. With the same diameter and a different pitch the nut starts, then jams after a turn or two, and forcing it damages both threads. Change the nut to the pitch of the bolt, or fit a coarse-to-fine adapter where neither part can change.
EKINSUN — a custom parts manufacturer that makes coarse-to-fine thread adapters, couplings and studs, and nuts and bolts in any ISO 261 fine pitch or inch thread, from 1 piece. Send the two threads, the length and the material; quote in 12 hours.