EKINSUN LTD is a custom parts manufacturer that makes cast parts to drawing or from a sample — pump casings and impellers, valve bodies and bonnets, bearing housings and pillow blocks, gearbox housings, motor end shields, flywheels, pulleys, handwheels, machine beds and bases, brackets and manifolds — in grey iron, ductile iron, cast steel, stainless steel, aluminium, bronze and aluminium bronze, machined after casting, from 1 piece. The tables list the parts by name: what each is also called, where it sits, what it is usually cast in and which faces are machined afterwards. How it is made — pattern and sand casting, a 3D-printed sand mould, investment casting, or machining from solid — is ours to choose by quantity, size and material.
Cast parts by name — what is cast, in which material, and what is machined afterwards
Seven families, more than fifty part names. Each row names the part the way buyers and manuals name it, and the faces that carry the accuracy: a casting is two jobs, the rough shape and the machining of the faces that fit, seal, locate or carry a bearing.
Pumps
A pump casing is usually cast in grey iron EN-GJL-250, ductile iron, CF8M or bronze, and after casting only the flange faces, the wear-ring and the seal-chamber bores are machined.
| Cast part — also called | Where it is used | Usual cast material | Machined after casting |
|---|---|---|---|
| Pump casing — volute casing, pump housing, pump body | centrifugal, end-suction, sewage, fire and process pumps — pump parts | grey iron EN-GJL-250, ductile iron, CF8M, bronze | flange faces, wear-ring and seal-chamber bores, bolt holes |
| Impeller — closed, open, semi-open, vortex | pumps, blowers, mixers | bronze CC491K, CF8M, grey iron, aluminium bronze | hub bore and keyway, wear-ring diameter, balancing |
| Pump cover — back plate, suction cover, casing cover | end-suction and split-case pumps | grey iron, CF8M | spigot, seal face, bolt holes |
| Bearing bracket — bearing frame, power frame, adapter | between the pump and the motor | grey iron | bearing bores in line, spigot faces |
| Stuffing box — seal chamber, gland, gland follower | shaft seals of pumps and valves — packing glands | bronze, grey iron | gland bore, stud holes |
| Gear pump body — hydraulic pump housing, end plate | hydraulic and oil gear pumps | grey iron EN-GJL-250 or 300, aluminium | gear bores, faces lapped flat |
| Diffuser, bowl, stage casing | vertical turbine and multistage pumps | bronze, grey iron | bores, spigots |
Need cast parts in a size, thread or material no catalogue lists? EKINSUN is a custom parts manufacturer: we make cast parts to your drawing, sketch or sample — grey iron, ductile iron, cast steel, CF8M stainless or aluminium — from 1 piece, quoted in 12 hours and shipped duties paid. Already a catalogue size? Ask us too — we may have it in stock, and larger quantities cost less per piece. How ordering without CAD works →
Valves
A valve body is cast in ductile iron, WCB, CF8M, bronze or forging brass; the ports, seats, flange faces and bonnet thread are machined after casting.
| Cast part — also called | Where it is used | Usual cast material | Machined after casting |
|---|---|---|---|
| Valve body — gate, globe, check, butterfly, ball, pressure reducing | pipelines, water mains, process plant — valve bodies | ductile iron, WCB, CF8M, bronze, forging brass | ports, seats, flange faces, bonnet thread |
| Valve bonnet — cover, yoke, top works | gate and globe valves | as the body | stem bore, packing chamber, bonnet flange |
| Butterfly disc, gate wedge, check disc — clapper, plate | inside the valve | ductile iron, CF8M, aluminium bronze | seat edge, shaft bore |
| Y-strainer body — basket strainer, pot strainer | ahead of pumps, meters and control valves | ductile iron, WCB, CF8M, bronze | screen seat, cap thread, flange faces |
| Hydrant body — standpipe head, fire valve, landing valve | fire and municipal water | ductile iron, bronze | outlet threads, seats |
Motors, gearboxes and drives
A gearbox housing is cast in grey iron EN-GJL-250, ductile iron or aluminium, and its bearing bores are machined in line after casting.
| Cast part — also called | Where it is used | Usual cast material | Machined after casting |
|---|---|---|---|
| Gearbox housing — gear case, reducer housing, transmission case | worm, helical and bevel reducers; machine drives — gearbox parts | grey iron EN-GJL-250, ductile iron, aluminium | bearing bores in line, split face, oil ports |
| Gearbox cover — inspection cover, bearing cap, end cover | gearboxes and reducers | grey iron, aluminium | face, spigot, bolt holes |
| Motor frame — stator housing, motor housing | electric motors | grey iron, aluminium | stator bore, feet, terminal-box face |
| Motor end shield — end bell, end cover, end bracket | both ends of an electric motor | grey iron, aluminium | bearing seat, spigot |
| Bearing housing — pillow block, plummer block, flange housing, take-up housing | conveyors, fans, farm machinery — custom housings | grey iron, ductile iron, cast steel | bearing bore, base face, bolt slots |
| Pulley — sheave, V-belt pulley, flat-belt pulley | belt drives | grey iron | bore, keyway, grooves |
| Flywheel | engines, presses, crushers, compressors | grey iron, ductile iron, cast steel | bore, faces, ring-gear seat, balancing |
| Coupling hub — flange coupling half, jaw coupling half | shaft couplings — shaft couplings | grey iron, ductile iron | bore, keyway, bolt circle |
| Worm wheel rim — bronze gear blank | worm gearboxes — worm gears | tin bronze CuSn12 (CC483K) | teeth cut after casting, hub bore |
| Handwheel — crank, lever, hand crank | valves, machine tools, presses | grey iron, ductile iron, aluminium | hub bore, square or keyway |
Machine tools and industrial equipment
A lathe, grinder or milling-machine bed is cast in grey iron EN-GJL-300, and its guideways are ground or scraped after casting.
| Cast part — also called | Where it is used | Usual cast material | Machined after casting |
|---|---|---|---|
| Machine bed — lathe bed, grinder bed | lathes, grinders, milling machines | grey iron EN-GJL-300 | guideways ground or scraped |
| Column, base, saddle, table, knee, carriage | milling, drilling and boring machines | grey iron | ways, T-slots, bores |
| Headstock and tailstock housing | lathes | grey iron | spindle bores in line |
| T-slot table, angle plate, riser block | workshops, fixtures, inspection | grey iron | faces ground or scraped, T-slots |
| Vice body — clamp body, jaw body | machine vices and clamps | ductile iron | jaw seats, slideway |
| Press frame — crown, bolster, slide | mechanical and hydraulic presses | cast steel, ductile iron | faces, bores |
| Mounting base — pedestal, bracket, robot base, motor base | machines, robots, instruments — robot parts | ductile iron, cast steel, aluminium | mounting faces, bolt holes |
| Fan housing — blower casing, scroll, inlet cone | ventilation, dust extraction, burners | grey iron, aluminium | flange faces, bearing seats |
Vehicles, construction and farm machinery
A differential carrier for a truck, tractor or classic car is cast in ductile iron or cast steel, with the bearing bores and flange faces machined.
| Cast part — also called | Where it is used | Usual cast material | Machined after casting |
|---|---|---|---|
| Differential carrier — axle housing end, final-drive housing | trucks, tractors, classic cars | ductile iron, cast steel | bearing bores, flange faces |
| Transmission case — bell housing, clutch housing | classic and commercial vehicles | aluminium, grey iron | bores, faces, dowel holes |
| Exhaust manifold | classic engines, generator sets | grey iron, high-silicon ductile iron | port faces, stud holes |
| Water pump housing, thermostat housing, oil filter housing | engines | aluminium, grey iron | sealing faces, bores, threads |
| Leaf spring hanger — shackle bracket, spring eye bracket | trailers, trucks, classic cars — spring hangers | ductile iron, cast steel | pin bores, bolt holes |
| Counterweight | forklifts, excavators, cranes, tractors | grey iron | mounting faces, bolt holes |
| Hydraulic valve housing — cylinder end cap, trunnion, gland | excavators, loaders, farm hydraulics — manifold blocks | ductile iron, cast steel | bores, ports, O-ring grooves |
| Tractor housings — gear housing, rear axle housing, PTO housing | tractors and farm machinery | grey iron, ductile iron | bearing bores, faces |
| Hub — wheel hub, implement hub, spindle housing | farm implements, industrial trailers | ductile iron | bearing seats, stud holes |
| Plough and tillage parts — frog, share holder, tine clamp | ploughs, cultivators, harrows | ductile iron, cast steel | bolt holes, fitting faces |
Marine, mining and energy
A seawater pump casing on board is cast in bronze CC491K or aluminium bronze, and a small-craft propeller in aluminium bronze CC333G or bronze, machined at the bore taper and keyway.
| Cast part — also called | Where it is used | Usual cast material | Machined after casting |
|---|---|---|---|
| Propeller and impeller (small craft, seawater pumps) | boats, cooling-water pumps | aluminium bronze CC333G, bronze | bore taper, keyway, balancing |
| Seawater pump casing — strainer body, sea cock body | engine cooling, bilge, fire pumps on board | bronze CC491K, aluminium bronze | flanges, ports |
| Bollard, cleat, fairlead — mooring fittings | decks and quays | ductile iron, CF8M, bronze | base holes |
| Crusher housing — bearing housing, flywheel, pulley (mining) | crushers, screens, conveyors | cast steel, ductile iron | bores, faces |
| Turbine housing, burner housing, generator base | energy plant and engines — turbo housings | ductile iron, cast steel, CF8M, aluminium | flanges, bores, faces |
Pipework, food and chemical plant, streets and furniture
Stainless pump bodies, valve bodies and sanitary fittings for food, dairy, chemical and pharma plant are cast in CF8M (1.4408) or CF3M (1.4409), with the ports and seats machined and the internals polished.
| Cast part — also called | Where it is used | Usual cast material | Machined after casting |
|---|---|---|---|
| Flange, reducer, bend, tee, cross (large or special angle) | pipelines, water mains, pump stations | ductile iron, cast steel, CF8M | flange faces, bolt holes |
| Stainless pump body, valve body, sanitary fitting body | food, dairy, chemical and pharma plant | CF8M (1.4408), CF3M (1.4409) | ports, seats, polished internals |
| Mixer and agitator hub — paddle hub, impeller hub | tanks and reactors | CF8M | bore, keyway |
| Manhole cover, gully grate, tree grate | streets, drains, car parks | grey iron, ductile iron (EN 124 load classes) | seat faces |
| Lamp post base, bollard, bench end, railing post | streets, parks, restoration | grey iron, aluminium | mounting holes |
| Cast iron table base — table legs, lamp base, gate ornament | furniture, restoration, decoration | grey iron, aluminium, bronze | little or none |
| Large hinge, gate pivot, structural connector | gates, doors, buildings — hinges | ductile iron, CF8M | pin bores, mounting faces |
The same cast parts in German, French and Spanish
A pump casing is a Pumpengehäuse or Spiralgehäuse in German, a corps de pompe or volute in French and a carcasa de bomba or voluta in Spanish; a valve body is a Ventilgehäuse, a corps de vanne and a cuerpo de válvula.
| English | German | French | Spanish |
|---|---|---|---|
| pump casing | Pumpengehäuse, Spiralgehäuse | corps de pompe, volute | carcasa de bomba, voluta |
| impeller | Laufrad | roue, turbine | impulsor, rodete |
| valve body | Ventilgehäuse | corps de vanne | cuerpo de válvula |
| bearing housing, pillow block | Lagergehäuse, Stehlager | corps de palier, palier | soporte de rodamiento, chumacera |
| gearbox housing | Getriebegehäuse | carter de réducteur | carcasa de reductor |
| motor end shield | Lagerschild | flasque moteur | tapa de motor |
| flywheel | Schwungrad | volant d’inertie | volante de inercia |
| pulley | Riemenscheibe | poulie | polea |
| handwheel | Handrad | volant de manœuvre | volante de maniobra |
| machine bed | Maschinenbett | banc, bâti de machine | bancada |
| exhaust manifold | Abgaskrümmer | collecteur d’échappement | colector de escape |
| counterweight | Gegengewicht | contrepoids | contrapeso |
How the part is made — pattern, printed sand mould, investment casting or machined from solid
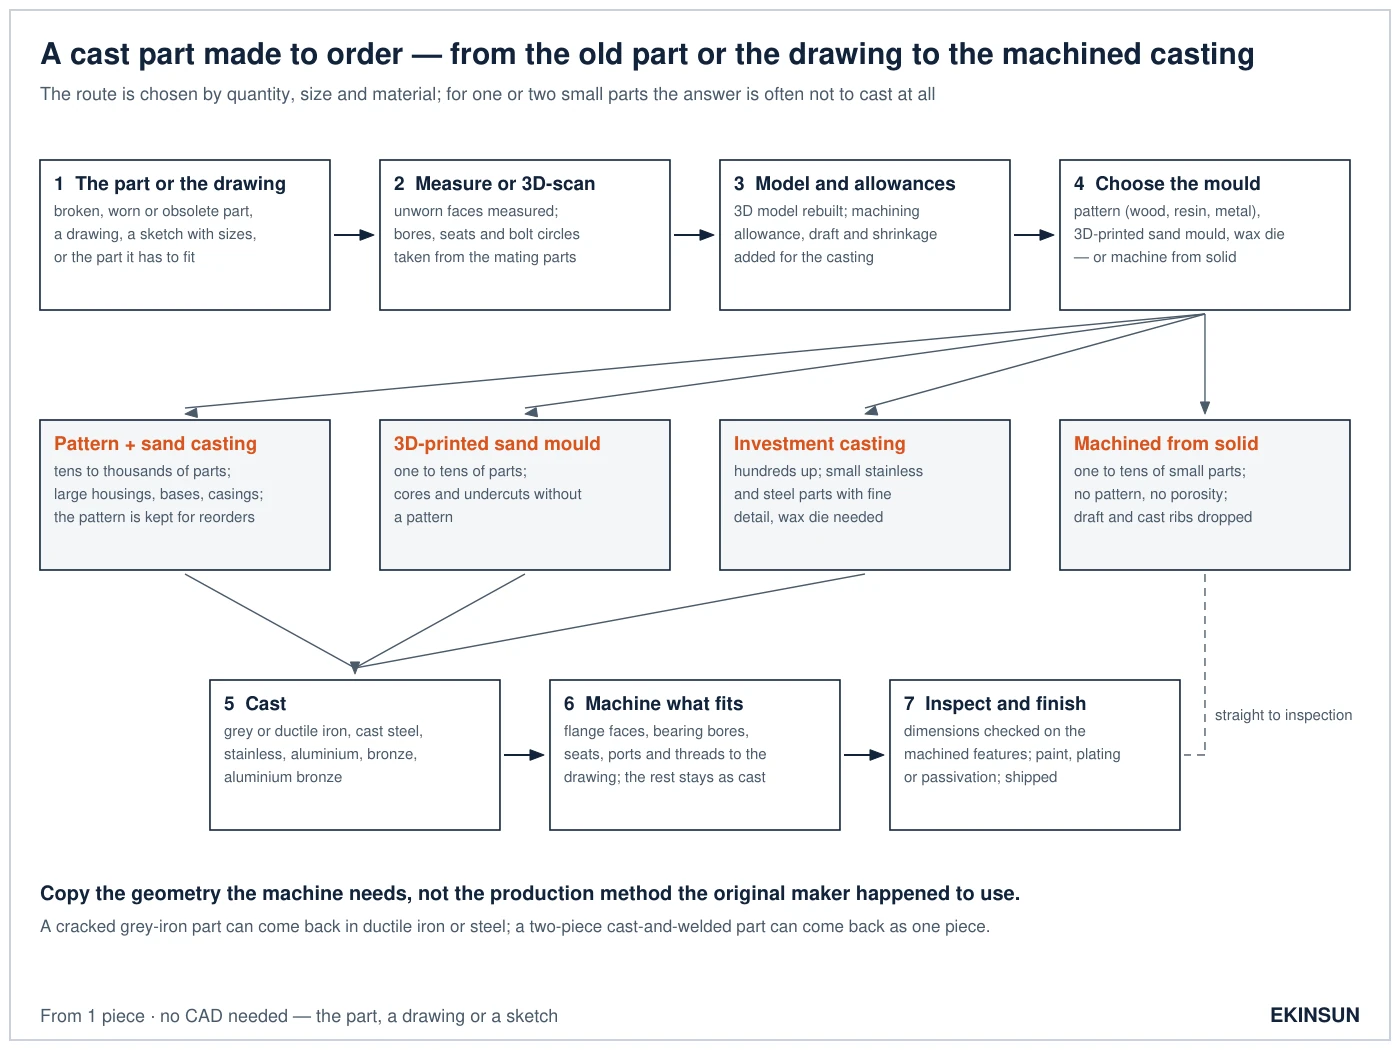
One to tens of pieces are machined from solid or cast in a 3D-printed sand mould, with no tooling; tens to thousands go to a pattern and sand casting at Ra 6.3–25 µm, and hundreds and up to investment casting at Ra 1.6–6.3 µm.
| Route | Tooling | Quantity it suits | Size and shape | Surface and accuracy | When it is chosen |
|---|---|---|---|---|---|
| Machined from solid bar, plate or block | none | one to tens | fits in a bar, plate or block | machined all over | small brackets, covers and bodies; no porosity; cast ribs and draft dropped where they had no function |
| 3D-printed sand mould | none — the mould is printed from the 3D model | one to tens | medium parts with cores and undercuts | as sand casting | an obsolete housing or casing needed a few times, no pattern |
| Pattern and sand casting | wood, resin or metal pattern and core boxes | tens to thousands | large parts, heavy sections | Ra 6.3–25 µm; coarse ISO 8062-3 grades | housings, bases and casings in series; the pattern is kept for reorders |
| Investment casting (lost wax) | wax injection die | hundreds and up | small to medium, fine detail | Ra 1.6–6.3 µm; finer grades | stainless and steel bodies, impellers, detailed brackets |
| Die casting | steel die | thousands and up | small to medium, thin walls | fine; ejector-pin marks | aluminium and zinc housings in series |
| Weld fabrication | none | one to tens | large frames, bases, brackets | machined after stress relief | a cast base or frame with no pattern and no reason to be cast |
Quantities are where each route usually pays; size, material and delivery move the boundaries. The quote names the route and the reason.
The rule behind the table: copy the geometry the machine needs, not the production method the original maker happened to use. A grey-iron bracket that cracked can come back in ductile iron or steel; a small cast cover needed twice is machined from a plate; a casting that was cast and welded in two parts can come back as one.
Is my part cast? How to tell a casting from a forging or a machined part
How can you tell if a metal part is cast?
A metal part is cast when it shows a parting line around it, draft on the walls, rounded edges, raised lettering and a grainy or finely pitted surface (Ra 6.3–25 µm on a sand casting), while only its flange faces, bores and threads are bright and machined. Pump casings, valve bodies, gearbox and bearing housings, motor end shields, flywheels, pulleys and machine beds are cast this way.
How can you tell if a part is cast or forged?
A cast part has a parting line with draft on both sides, a grainy surface and raised cast lettering; a forged part has a smoother, scaled surface, a trimmed flash line round its widest point and stamped lettering, and a cut and etched section shows grain flow that follows the shape. Forgings are solid and have no internal passages; castings often do.
How can you tell cast iron from cast steel, stainless or aluminium?
A magnet sticks firmly to cast iron and cast steel, weakly or not at all to cast austenitic stainless, and not at all to aluminium, brass or bronze. Grey cast iron breaks with a dark grey granular fracture and makes a dull sound when tapped; cast steel rings and bends before it breaks; aluminium is about one third of the weight of iron for the same size.
Which parts are usually cast?
Parts with curved walls, internal passages, ribs or thick and thin sections in one piece are usually cast, because machining that shape from solid would take hours and turn most of the bar into chips. The tables above list more than fifty of them by name, with the material they are usually cast in and the faces machined afterwards.
Can a cast part be made again when the maker no longer sells it?
Yes. A cast part is copied from the part or its pieces: measured or 3D-scanned, the model rebuilt with draft and machining allowance, cast from a pattern or a 3D-printed sand mould, and machined on the faces that fit; one or two small parts are machined from solid instead. EKINSUN makes these from 1 piece, from the part, a drawing or a sketch.
| What you see | Sand cast | Investment cast | Die cast | Forged | Machined from solid |
|---|---|---|---|---|---|
| Surface | grainy sand texture, Ra 6.3–25 µm | smooth, fine texture, Ra 1.6–6.3 µm | smooth, ejector-pin marks | smooth with scale; flow lines on a cut face | tool marks all over |
| Parting line | visible, often ground | faint or none | sharp line, trimmed flash | flash line trimmed round the part | none |
| Draft on walls | yes | little | yes, small | yes | none |
| Edges and corners | rounded | fine detail possible | crisp, thin walls | rounded | sharp |
| Lettering, part numbers | raised, soft-edged | raised, crisp | raised, crisp | stamped | engraved |
| Usual materials | iron, steel, bronze, aluminium | steel, stainless, brass | aluminium, zinc, magnesium | steel, brass, aluminium | any bar or plate |
The faces that are bright and flat, the bores and the threads are machined whichever way the part was made; the question that matters for a copy is what the rest of the shape does. Raised part numbers on a housing often name the original maker and the pattern, which helps find the drawing or the grade.
Cast materials — grey iron, ductile iron, cast steel, stainless, aluminium and bronze
Grey iron EN-GJL-250 is GG-25 in old DIN, A48 Class 35 in ASTM, HT250 in China and FC250 in Japan; ductile iron EN-GJS-400-15 is GGG-40, A536 60-40-18, QT400-15 and FCD400.
| Material | EN · old DIN · ASTM · China GB · JIS | Where it fits |
|---|---|---|
| Grey iron | EN-GJL-250 · GG-25 · A48 Class 35 · HT250 · FC250 | housings, beds, bases, pump casings, pulleys; damps vibration, machines well, brittle |
| Grey iron, stronger | EN-GJL-300 · GG-30 · A48 Class 45 · HT300 · FC300 | machine beds and gear housings |
| Ductile iron | EN-GJS-400-15 · GGG-40 · A536 60-40-18 · QT400-15 · FCD400 | valve bodies, hubs, brackets and housings that take shock |
| Ductile iron, higher strength | EN-GJS-500-7 · GGG-50 · QT500-7 · FCD500 | gears, heavy housings, press parts |
| Cast carbon steel | GP240GH (1.0619) · GS-C25 · A216 WCB · ZG230-450 · SCPH2 | valve bodies, heavy brackets, press frames; weldable |
| Cast stainless 316 | 1.4408 · A351 CF8M · SCS14 | pumps and valves in chemicals, food and seawater |
| Aluminium | EN AC-42100 (AlSi7Mg0.3) · G-AlSi7Mg · A356 · ZL101A · AC4C | light housings, covers, manifolds, marine fittings |
| Bronze (gunmetal) | CC491K (CuSn5Zn5Pb5-C) · Rg5 · C83600 | pump and valve bodies in water, bushings |
| Tin bronze | CC483K (CuSn12-C) · G-CuSn12 | worm wheels, heavy bushings |
| Aluminium bronze | CC333G (CuAl10Fe5Ni5-C) · G-CuAl10Ni · C95800 | seawater pumps, propellers, impellers, valve discs |
| Bar, when the part is machined from solid | 304 (1.4301), 316L (1.4404), 6061-T6, 7075-T6, C45, 42CrMo4 | brackets, covers, bodies and bases machined instead of cast |
Nearest equivalents, not identical chemistries; the drawing or order names one standard. Grey and ductile iron grade by grade, with the ASTM grade each one meets: cast iron vs ductile iron.
Tolerances, machining allowance and why a casting needs the part or a drawing
A raw casting is not held to machining tolerances. ISO 8062-3 grades casting tolerances from DCTG 1 to DCTG 16 by process and material: sand castings sit in the coarse grades, investment and die castings in the finer ones, and a machining allowance is added to every face that will be machined. Every face that fits, seals, locates or carries a bearing is machined afterwards to the drawing or to ISO 2768.
Draft angles, fillet radii, machining allowance and shrinkage are built into the model before a pattern or printed mould is made. That is why a housing, cover or casing cannot be made from a few dimensions: the part itself, the pieces of a broken one, or a drawing is needed. Bores, bolt circles and seats are taken from the faces that did not wear, or from the mating parts.
What to send for a cast part
- The part, or the pieces of a broken one; or a drawing; or photos of every face with a ruler in the picture, so we can say which route fits before you ship.
- What it bolts to and what runs in it: the shaft, the bearing, the pipe flange, the gear.
- The material if known — cast marks, the maker’s part number, or the machine it comes from.
- Quantity now and later: one replacement, a few spares, or a series.
- Anything that failed: a crack, a worn bore, a corroded seat — so the copy can be stronger than the original.
Where the catalogue stops
A cast part the equipment maker still sells is best bought from the maker; an obsolete, cracked or worn one with no drawing is copied from the part, cast from a pattern or a printed mould, then machined.
| What you need | In the catalogue? | What we make |
|---|---|---|
| A cast part the equipment maker still sells | Yes | Buy it from the maker; no one-off competes on price with a series casting. Standard parts: ask us too — we may have them in stock. |
| The same cast part, obsolete, cracked or worn, with no drawing | No | Copied from the part: measured or scanned, model rebuilt, cast from a pattern or a printed mould, then machined. |
| One or two pieces of a small bracket, cover or block | Partly | Usually machined from solid instead of cast — no pattern cost, no porosity. |
| A large housing, base or casing in grey or ductile iron, one to ten pieces | No | Printed sand mould or a wood pattern, cast, and machined on the faces that fit. |
| A cast part in a stronger grade than the original — grey iron to ductile iron, bronze to aluminium bronze | No | Cast in the grade you choose; the original grade is kept on the drawing when it is known. |
| Stainless pump or valve bodies with internal passages | Partly | Investment cast in CF8M (1.4408) for a series; one piece is machined from bar or cast in a printed mould. |
| Standard pipe fittings, manhole covers, gratings and hydrant bodies | Yes | Buy standard products from pipe and municipal suppliers; we make the non-standard sizes and the obsolete patterns. |
| A casting with a pressure rating, PED or CE marking, or a certification chain | Partly | The material certificate for each melt comes with the casting; product approvals belong to the maker of the finished product, and we say before quoting what comes with the part. |
Related pages
- Valve bodies — pressure reducing, gate, globe, check, butterfly and ball valve bodies
- Pump replacement parts — impellers, shafts, wear rings and casings
- Custom housings — bearing housings and machined enclosures
- Gearbox parts — gears, shafts and housings for gearboxes
- Manifold blocks — hydraulic and pneumatic blocks machined from solid
- Copying a cast part without drawings — how the shape is captured and rebuilt
- Obsolete parts — parts copied when the maker is gone
- Billet aluminium blocks — why some parts are machined from solid instead of cast
A bearing housing in 1 to 10 pieces is machined from block rather than cast; UCP 204 to 212 sizes and the dimensions a replacement keeps are on bearing housing replacement.
Frequently asked questions
Yes, three ways: machine the part from solid, with no pattern, when it fits in a bar or plate; cast it in a 3D-printed sand mould, with no pattern, when it has cores or undercuts; or make a wood or resin pattern and sand cast it, and keep the pattern for later orders. Which is cheapest depends on size, shape and how many will follow.
Sand castings have a grainy surface (Ra 6.3-25 µm), a parting line and draft on the walls; investment castings are smoother (Ra 1.6-6.3 µm) with fine detail and little draft; forgings are smooth with a trimmed flash line and stamped, not cast, lettering. Machined faces, bores and threads look the same on all three.
Sand casting forms the mould in sand around a pattern and suits large parts, grey and ductile iron and any quantity from one printed mould up; investment casting pours metal into a ceramic shell built on a wax model and suits small steel and stainless parts with fine detail and a smoother surface, but needs a wax injection die.
Yes, when the part or its pieces are sent: the shape is measured from the unbroken faces, the model is rebuilt and the new part is cast from a pattern or printed mould and machined. Where grey iron cracked, the copy can be made in ductile iron or steel, or machined from solid when it is small.
Raw sand-cast surfaces are toleranced to the coarser ISO 8062-3 casting grades, so every face that fits, seals, locates or carries a bearing is machined after casting to the drawing or to ISO 2768; the rest of the shape stays as cast.
A drawing or the part itself. Housings, covers and casings cannot be made from a few dimensions, because draft, wall thickness and cores decide the shape; photos of every face with a ruler let us say which route fits before the part is shipped.
EKINSUN LTD is a custom parts manufacturer that makes cast parts to drawing or from a sample - pump casings, impellers, valve bodies, bearing and gearbox housings, motor end shields, flywheels, pulleys, handwheels and machine bases - in iron, steel, stainless, aluminium and bronze, cast and machined, from 1 piece, with a quote within 12 hours.
No list price. A cast part costs the pattern or mould once, plus metal, pouring and machining for each piece; at one or two pieces the pattern dominates, which is why small parts are often machined from solid instead. The quote names the route and what each part of the price is for.
Send the part or the drawing
Photos of every face with a ruler, the broken pieces if it cracked, or a drawing; the material if known, what it bolts to, and the quantity. From 1 piece, quote within 12 hours.
Castings, housings and covers cannot be made from a few dimensions: send the part, the pieces of a broken one, or a drawing. Photos of every face with a ruler let us say which route fits before you ship anything.